Skip to content

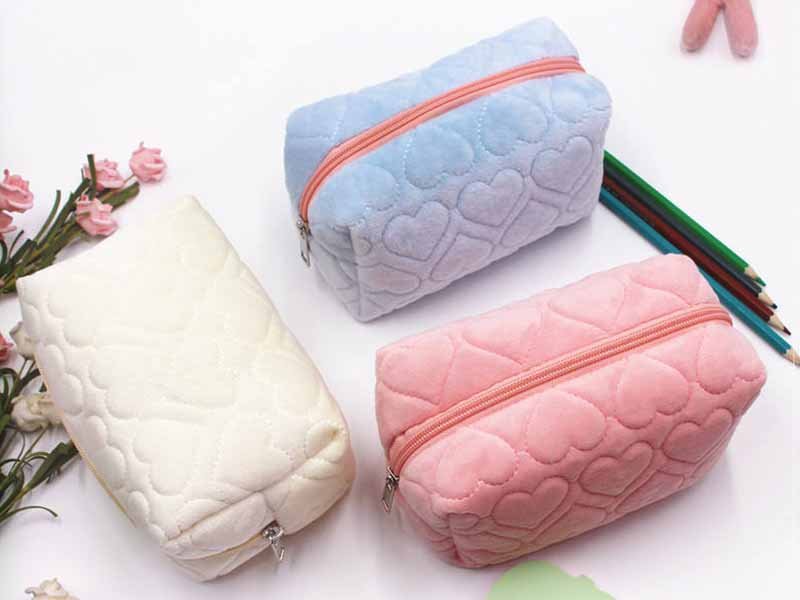
A cosmetic bag looks simple until you need thousands of them to look, feel and perform the same way. A zipper pouch may contain only a few visible components, yet small decisions about fabric thickness, lining, zipper length, pocket position, reinforcement and logo application can completely change the finished product. Those decisions also affect material purchasing, sampling time, minimum order quantities, sewing efficiency, inspection standards, packaging volume and ultimately the price paid for every finished unit.
Custom cosmetic bag manufacturing is the process of turning a concept, reference product, drawing, tech pack or physical sample into a repeatable product specification and then controlling materials, patterns, sampling, branding, sewing, quality inspection, packaging and shipment around that standard. Successful projects are not simply about putting a logo on an existing pouch. They connect product function, brand positioning, target cost, order quantity and manufacturing practicality before bulk production begins.
That distinction becomes important when a product moves from one prototype to 500, 5,000 or 50,000 pieces. Imagine approving an attractive sample for a new skincare launch and later discovering that the production zipper opening is 20 mm narrower, several bottles no longer fit comfortably, and the lining wrinkles when the bag is filled. None of those problems would necessarily make the product unusable, but together they can turn a promising launch into customer complaints, repacking work and avoidable cost. Good manufacturing is therefore less about fixing finished bags and more about eliminating uncertainty before those bags reach the sewing line.
How Are Custom Cosmetic Bags Made?

Custom cosmetic bags are normally manufactured through a controlled sequence that includes requirement review, material selection, structural development, pattern making, sampling, approval, bulk material preparation, cutting, logo application, sewing, inspection, packaging and shipment. The purpose of this sequence is to turn one approved design into a documented production standard that can be repeated consistently across the full order rather than relying on worker interpretation.
From Product Brief to Pattern
A factory can receive a message saying, “We need 1,000 black makeup bags with our logo,” and produce a quotation, but that quotation will inevitably contain assumptions. It may assume a standard polyester fabric, common zipper, basic lining and simple screen print. If the actual expectation is soft PU leather, reinforced construction, custom metal hardware and retail packaging, the original price becomes almost meaningless. Good development therefore begins by defining the intended product before discussing a final manufacturing price.
A useful brief should explain the finished dimensions, what the bag needs to hold, order quantity, number of colors, preferred materials, lining expectations, logo artwork, zipper style, internal compartments, packaging requirements, destination country and intended launch timing. A physical sample or reference image is useful, but visual references alone do not define construction. Two cosmetic bags can look nearly identical in photographs while using different foam thicknesses, zipper grades, lining fabrics and internal reinforcement.
Pattern making converts this commercial brief into manufacturable components. A 220 × 150 × 80 mm bag is not defined only by those three exterior measurements. The pattern must also account for seam allowances, zipper installation, gusset depth, lining allowance, foam or board thickness, binding, pocket position and assembly sequence. A change of only 5–10 mm around the zipper opening can noticeably improve access to bottles or brushes, while the same small change in pocket height can determine whether a palette stays secure or falls out during travel.
Before the first sample is made, the development team should normally confirm the following points:
- Finished width, height and depth
- Maximum usable zipper opening
- Zipper direction and number of sliders
- Internal pocket quantity and dimensions
- Lining material and construction
- Foam, board or structural reinforcement
- Handle, wrist strap or loop position
- Logo size, technique and location
- Packaging method and label requirements
The more clearly these items are defined, the less the project depends on assumptions. This is particularly valuable for repeat programs because the same information can later be used to compare suppliers, approve revisions and control future replenishment orders.
Sampling and Approval
Sampling is where drawings meet reality. Computer renderings can communicate proportion and color, but they cannot fully show how a zipper moves around a curved corner, how a PU surface wrinkles after turning, how thick foam changes the shape of a gusset or how easily the customer can reach a bottle positioned behind an internal divider. A physical sample therefore serves both as a design prototype and as an early manufacturing test.
The sample should be tested with the actual products it is intended to carry whenever possible. If a travel pouch is supposed to hold two 100 ml skincare bottles, a serum, foundation, compact and brush set, those items should be placed inside before approval. This quickly exposes problems that dimensional drawings may miss, such as insufficient opening width, unstable bottle positions or pockets that become inaccessible when the main compartment is full.
Sample comments are most useful when they are measurable. “Make the handle a little longer” creates interpretation risk, while “increase finished handle drop from 42 mm to 55 mm” gives the pattern and sewing teams a clear instruction. The same principle applies to logo dimensions, zipper opening, pocket placement and reinforcement.
| Development Item | First Sample | Approved Revision |
|---|---|---|
| Finished width | 220 mm | 220 mm |
| Zipper opening | 165 mm | 180 mm |
| Logo width | 62 mm | 52 mm |
| Inner pocket height | 70 mm | 85 mm |
| Handle drop | 42 mm | 55 mm |
| Foam thickness | 2 mm | 3 mm |
Szoneier’s development process can start from a tech pack, reference photograph, physical sample, sketch or early product idea. Material confirmation, pattern making, prototype sewing, internal review, photographs or video, sample shipment, revision and final approval are used to move the concept toward a production-ready reference. The important point is that the approved sample should not exist in isolation; it should be supported by written dimensions, material information and approved artwork so the production team knows exactly what must remain consistent.
Cutting, Sewing and Finishing
Bulk production begins with material preparation rather than with sewing. Main fabric, lining, foam, webbing, zipper tape, pullers, labels and hardware should be checked against the approved references before large quantities are cut. This is especially important with PU, coated fabrics and dyed textiles because two batches carrying the same general material description may still differ in surface grain, shade, stiffness or hand feel.
After materials are released, panels are cut according to the approved pattern. Some branding processes are completed while the pieces are still flat. Screen printing, heat transfer, embroidery and certain patch applications can often be positioned more accurately before assembly. Other components, such as metal plates, zipper pullers or labels, may be added later according to the sewing sequence.
The sewing sequence itself influences appearance and consistency. Cosmetic bags often combine several layers in relatively small spaces, making zipper ends, curves, lining attachment, pocket corners and binding particularly sensitive. Structured cases add another challenge because foam or board must remain correctly positioned while multiple layers are sewn together. If reinforcement moves during assembly, the finished bag can twist, lean or lose symmetry even when the exterior fabric has been cut correctly.
Finishing includes trimming threads, cleaning marks, shaping the product and checking zipper movement before final inspection. Soft products may require controlled folding or temporary stuffing to preserve their intended shape during packing. These details explain why quality cannot simply be added at the final inspection table. By the time a finished bag reaches that stage, the important decisions about materials, cutting, logo placement and construction have already been made.
Which Cosmetic Bag Materials Work Best?

There is no single material that is best for every cosmetic bag. Polyester and nylon are practical for lightweight functional designs, PU creates a polished fashion-oriented appearance, canvas offers a natural textile feel, while PVC and TPU can provide transparent or wipe-clean surfaces. The best choice depends on appearance, durability, cleaning requirements, structure, branding method, target price and how the finished product will actually be used.
Outer Material Options
Polyester remains one of the most flexible materials in commercial cosmetic bag production. It is available in many weaves, colors and surface treatments, works with numerous printing processes and can be used for both inexpensive promotional pouches and more structured travel products. The term “polyester,” however, describes a broad family of fabrics rather than one quality level, so density, yarn size, coating, hand feel and finishing should be evaluated during sampling.
Nylon is commonly selected for travel-oriented and more technical-looking bags because it can provide good abrasion performance while remaining relatively lightweight. Depending on the construction, nylon can feel smoother and more refined than standard polyester, although the material itself may cost more. High-density woven nylon is particularly useful when the product needs a cleaner surface and flexible structure without becoming bulky.
Canvas and cotton suit beauty, lifestyle and wellness brands that want a warmer, more natural textile appearance. Their visible weave works well with screen printing, embroidery, woven labels and simple brand graphics. The trade-off is cleanability. Untreated natural fabrics can absorb liquid foundation, oils and skincare products more readily than coated synthetic surfaces, making them less suitable for products expected to encounter frequent spills.
PU leather is frequently used when the product needs a more polished appearance. Surface grain, backing fabric, thickness, flexibility and coating quality all affect the finished result, and two materials both sold as “PU leather” can behave very differently during sewing. A supple PU may produce elegant folds in a soft pouch, while a heavier structured PU can work better for vanity cases that need to stand upright.
PVC and TPU are widely used for transparent cosmetic pouches or clear panels. Material thickness requires careful consideration because a film that is too thin may wrinkle excessively, while a thick film can become difficult to turn and sew around tight curves. Neoprene is another useful option when softness, cushioning and stretch matter, although its thickness increases product volume and packing density.
| Material | Typical Application | Key Advantage | Important Consideration |
|---|---|---|---|
| Polyester | Everyday, promotional, travel | Flexible cost and print options | Performance varies by weave/coating |
| Nylon | Travel, functional, premium casual | Lightweight and abrasion resistant | Usually costs more than basic polyester |
| Cotton/Canvas | Natural and lifestyle collections | Strong textile character | More vulnerable to spills |
| PU | Fashion and premium beauty | Clean, polished appearance | Surface quality varies substantially |
| PVC/TPU | Transparent and wipe-clean bags | Visibility and easy cleaning | Thickness affects construction |
| Neoprene | Protective soft pouches | Cushioning and stretch | Higher volume and weight |
| RPET | Recycled-material programs | Sustainability positioning | Documentation should be verified |
Rather than asking for the cheapest fabric, it is usually more productive to describe the expected finished result. A supplier can then compare several materials at different price levels while keeping the intended hand feel, structure and appearance in view.
Lining and Spill Resistance
Lining deserves more attention in cosmetic bags than it receives in many product briefs because the category naturally carries powders, creams, lotions, oils and liquids. A beautiful exterior loses much of its value if a small spill permanently stains the interior or if a lightweight lining tears around the pocket seam after several months of use.
Standard polyester lining remains widely used because it is lightweight, stable and economical. For products expected to carry liquid foundation, skincare bottles or toiletries, smoother coated or laminated materials may provide easier cleaning. However, a wipeable lining should not automatically be described as making the entire bag waterproof. Needle holes, seams and zipper openings can still allow liquid to escape unless the construction has specifically been engineered and tested for waterproof performance.
A useful lining specification should include more than a generic fabric name. Composition, approximate weight, surface coating, color, texture, cleanability and compatibility with pockets or reinforcement should all be considered. Very thin lining can save material cost but may wrinkle noticeably, show seam allowances or tear under repeated tension. A heavier lining can improve hand feel and durability but may also increase bulk around seams and corners.
For structured cases, lining should be considered together with foam, board or other reinforcement. A combination that appears appropriate when materials are handled separately may become too thick once several layers are sewn around a zipper or bound edge. Testing these combinations during sampling is usually much more reliable than trying to judge them from swatches alone.
Sustainable Material Choices
Sustainability requirements are becoming more common in beauty accessories, but meaningful claims require more detail than replacing the outer fabric with something described as recycled. RPET polyester can support recycled-content programs, while organic cotton and other certified materials may be appropriate for natural or wellness-focused brands. The commercial challenge is establishing exactly which parts of the finished product are covered by the claim and whether supporting documentation is available.
A cosmetic bag can include outer fabric, lining, foam, zipper tape, thread, labels, webbing, patches and packaging. If only the outer shell contains recycled material, marketing language should reflect that reality. Companies with formal sustainability policies may also need supplier documentation, chain-of-custody information or certificates that correspond to the actual production material rather than to a similar fabric held by the supplier.
Useful questions include:
- What percentage of the finished product uses the claimed material?
- Is documentation available for the exact production fabric?
- Does certification cover the material or the finished product?
- Are custom colors available within the same certified program?
- Does custom dyeing change the material MOQ?
- Can the same material be sourced for future reorders?
- Does the alternative affect durability, weight or cleaning performance?
Sustainability should also be considered over the useful life of the product. A bag made from a recycled material but designed with weak stitching or an unreliable zipper may need replacement sooner than a more durable alternative. Material choice, construction quality, packaging volume and long-term usability therefore belong in the same discussion rather than being treated as separate issues.
What Can You Customize?

A custom cosmetic bag can be developed around size, shape, outer material, lining, pockets, dividers, zippers, hardware, colors, logo treatments, labels and packaging. Effective customization is not about making every component unique. It is about concentrating development effort on details customers will notice, use and associate with the brand while standardizing less visible components when that helps control cost, MOQ and repeat-production complexity.
Size, Shape and Function
The term “cosmetic bag” covers a surprisingly broad range of constructions. A flat zipper pouch is practical for gift-with-purchase programs and small everyday products. A bottom gusset provides additional capacity without dramatically increasing production complexity. Wide U-shaped openings improve access, while structured vanity cases provide stronger presentation and can protect bottles more effectively. Hanging toiletry bags, brush organizers and clear travel pouches serve entirely different use cases despite belonging to the same general category.
Common styles include:
- Flat zipper pouches
- Bottom-gusset cosmetic bags
- Box-shaped makeup bags
- Double-zip cases
- Wide U-opening vanity cases
- Structured train cases
- Brush organizers
- Hanging toiletry bags
- Clear travel pouches
- Drawstring beauty pouches
The correct dimensions should normally be developed around the contents rather than copied from a competitor product. If a bottle is 175 mm tall, specifying exactly 175 mm of internal height may not provide enough usable space because lining, seam allowances, reinforcement and zipper construction all reduce the practical interior dimensions. A small amount of clearance can make the difference between an item fitting comfortably and the customer needing to force the zipper closed.
Internal design also needs physical testing. Elastic loops should hold brushes securely without making them difficult to remove. Mesh pockets need enough opening width for the products they are expected to carry. Dividers should maintain their position when the bag is partly loaded rather than only when it is completely full. Testing a sample in both empty and loaded conditions gives a much more realistic picture of how the finished product will perform.
Logo and Branding Methods
Branding methods should be selected according to material surface, artwork complexity, order quantity and intended visual position. Screen printing remains efficient for simple graphics on suitable fabrics, while heat transfer supports detailed or multicolor designs. Digital and sublimation printing can handle more complex visual artwork, and embroidery adds texture when the base material is stable enough to support repeated needle penetration.
Woven labels provide a consistent branding method across different fabrics. Rubber, silicone and TPU patches create a more casual or technical appearance. Metal plates can make a product look more premium but add component sourcing and attachment requirements. Debossing, hot stamping and similar surface techniques work well on selected PU and leather constructions where the material accepts the impression cleanly.
Szoneier supports a broad range of branding processes, including screen printing, heat transfer, digital printing, sublimation, embroidery, woven labels, leather patches, rubber and silicone patches, metal plates, debossing, hot stamping, laser engraving, TPU patches, jacquard webbing and custom zipper pullers. The suitable process depends not only on appearance but also on material, artwork detail, MOQ, durability and the stability of the technique in bulk production.
Artwork should always be evaluated at actual production size. A wordmark with very fine strokes may look excellent on a computer screen and lose definition when reduced to 30 or 40 mm in embroidery. A metal logo plate that looks subtle in a rendering can visually dominate a small pouch once it is produced. These issues are easier to correct during artwork review and sampling than after custom components have already been ordered.
Zippers and Internal Details
The zipper is often the most frequently handled component on a cosmetic bag, which makes its performance disproportionately important to the end-user experience. Customers may never know the exact fabric denier, but they immediately notice a zipper that catches, separates or requires too much force. Selection should therefore cover coil or tooth construction, tape width, slider quality, opening direction, puller size and the way the zipper ends are finished.
Custom zipper pullers can strengthen brand identity, particularly on premium or repeated product programs. They can also introduce additional tooling, component MOQ and development time. For an early-stage order, a reliable standard slider combined with a branded fabric tab, rubber attachment or carefully selected puller may provide a better balance between differentiation and supply-chain simplicity.
Internal organization should be developed around real products rather than simply adding pockets because competitors have them. A cosmetic bag containing several large bottles may benefit more from one stable divider than from five small pockets. A brush organizer requires different dimensions from a skincare travel case. The number and position of compartments can also increase sewing time because every pocket introduces additional cutting, alignment and stitching operations.
SKU planning deserves attention at this stage. A collection can offer six exterior colors while using two common linings, one zipper specification, one puller design and one internal construction. Customers still see six distinct products, but the factory manages fewer unique components. This kind of controlled standardization can reduce minimum purchasing quantities, simplify stock management and make repeat orders easier without sacrificing visible product differentiation.
How Do Sampling, MOQ, and Cost Work?
Sampling verifies whether the design works in physical form, MOQ reflects the minimum practical quantity for the selected materials and components, and cost reflects the complete construction rather than product dimensions alone. These factors are closely connected. Custom fabrics, molded hardware, complex compartments or premium packaging can increase development requirements, supplier minimums and unit cost even when the finished bag is similar in size to a basic pouch.
Sampling and Revision
The sample stage should answer more than the question of whether a bag looks attractive. It should verify dimensions, capacity, material behavior, zipper movement, lining construction, logo placement, internal organization and packaging compatibility. Structured products should also be checked for symmetry and reinforcement because foam or board can shift during sewing and change the final shape.
Feedback becomes more effective when it is organized into one revision document rather than distributed across unrelated messages. A useful internal review separates comments into items that must change, items that could be improved and items that are already approved. This helps the factory understand which details are critical and reduces the risk of modifying something the customer was already satisfied with.
Measurable feedback is particularly important. “Move the logo down” creates interpretation; “move the logo center 8 mm downward” creates an instruction. “Make the pocket bigger” can be understood several ways, while specifying a new finished width and height allows the pattern to be revised accurately.
Sampling should also consider repeatability. A decorative detail may look perfect when a highly experienced sample maker spends additional time positioning it, but if that detail is difficult to reproduce consistently at normal production speed, it can become a source of variation in bulk manufacturing. The best approved sample is therefore not only visually strong; it represents a construction that can be repeated on the production floor.
MOQ and SKU Planning
Minimum order quantity is influenced by several overlapping factors. The sewing line may be capable of producing a relatively small number of pieces, but the fabric mill, zipper supplier, hardware vendor or packaging printer may each have their own minimums. A custom bag containing several specially made components is therefore governed by the least flexible part of its supply chain rather than by sewing capacity alone.
Szoneier supports MOQ starting from around 200 pieces for many standard custom bag projects, including selected cosmetic pouches and makeup bags. This is generally most practical when projects use available materials, standard colors, common accessories and relatively straightforward branding. Custom-dyed fabrics, proprietary hardware, molded zipper pullers, complex retail boxes or unusual certified materials can require higher quantities depending on the component supplier.
SKU quantity also changes the economics. Consider three programs with the same total order size:
- 1 color × 2,400 pieces
- 4 colors × 600 pieces
- 8 colors × 300 pieces
All three orders contain 2,400 bags, but the final program requires more material matching, more packing labels, more production changeovers and potentially more minimum purchases from component suppliers. For a first launch, reducing unnecessary SKU variation can sometimes save more money than negotiating a few cents from the sewing price.
An efficient early collection might use three or four exterior colors while keeping the same lining family, zipper specification, internal structure and packaging format. This provides visible assortment variety while maintaining a simpler supply chain. Once demand becomes clearer, additional colors or feature variations can be added using the original approved platform.
Cost and Lead Time
Two cosmetic bags measuring 200 × 140 × 70 mm can have very different prices because size alone does not describe what must be purchased or sewn. A simple polyester pouch with a standard zipper, basic lining and one-color print may require relatively few production operations. A structured PU case of identical dimensions can include foam, piping, two pockets, custom hardware, debossing and a rigid retail box, creating a completely different material and labor profile.
The main cost drivers normally include:
- Outer material and material consumption
- Lining material
- Foam, board or reinforcement
- Number of cut panels
- Sewing complexity
- Zipper length and grade
- Custom hardware
- Logo technique
- Number of colorways
- Mold or setup charges
- Inspection requirements
- Individual packaging
- Retail packaging
- Testing requirements
- Total production volume
Price comparisons therefore need to be based on identical specifications. A quotation that is 10% lower may simply use a lighter lining, cheaper zipper or different material grade. Unless those differences are identified, the numbers cannot be compared fairly.
Lead time should also be considered as a sequence rather than one fixed production number. Requirement review, sourcing, first sampling, revisions, approval, bulk material booking, cutting, sewing, inspection and packing each consume time. Products made from available fabrics and standard components generally move more quickly than projects involving custom color development, molded hardware or printed presentation packaging.
For launches tied to a firm sales date, planning should work backward from warehouse arrival rather than from factory completion. Freight, customs clearance, warehouse appointments and distribution all occur after the manufacturing team finishes packing. Building a reasonable schedule around those real stages is more reliable than requesting an unrealistic production deadline and hoping later steps will somehow fit.
How Is Bulk Quality Controlled?

Bulk quality is controlled by comparing production against approved references at several points rather than waiting until every bag is finished. Effective systems combine material checks, component verification, pre-production confirmation, cutting inspection, in-line sewing checks, final inspection and packaging control. Detecting an incorrect zipper or logo position after 100 pieces is inconvenient; finding the same problem after 10,000 pieces can become a serious commercial issue.
Pre-Production Checks
Quality control starts with approved information and components. If the wrong lining shade reaches production, excellent sewing cannot correct it later. If a zipper supplier sends the wrong tape finish, final inspection can identify the error but cannot remove it economically from thousands of completed bags. Materials should therefore be compared against approved references before they are consumed.
A practical production reference includes the approved physical sample, dimension sheet, material references, color standard, logo artwork, branding position, zipper and hardware specification, pocket layout and packing instructions. Larger or more complex programs can benefit from a pre-production review in which cutting, sewing, quality and packaging teams confirm that they are working from the same version.
Material variation deserves particular attention. Two black fabrics can appear identical in warehouse lighting and look noticeably different under retail lighting or photography. PU surfaces can vary in grain or gloss. Hardware with the same color name may come from different plating batches. These variations are easier to manage when references and acceptable ranges have been agreed before the order is released.
The purpose of pre-production inspection is not to create bureaucracy. It is to stop predictable errors before they are multiplied. A few minutes spent verifying a zipper, material shade or logo file can save days of rework once sewing has begun.
Sewing and In-Line Inspection
In-line inspection focuses on the points where defects can still be corrected economically. Common cosmetic bag checkpoints include zipper alignment, corner shape, lining attachment, binding width, pocket location, reinforcement position, logo placement and stitch consistency. For structured cases, inspectors may also check whether foam, board or supporting layers have shifted during assembly.
The timing of these checks matters. A logo positioned incorrectly on a flat panel should ideally be identified before that panel is joined to the bag. A zipper that is too short should be corrected before the lining and binding are completed. The further a faulty component travels through the assembly process, the more labor has to be removed or discarded when the problem is discovered.
Functional testing should accompany visual inspection. Opening and closing the zipper repeatedly, checking pocket access, loading representative cosmetics and confirming that the bag sits correctly when filled can reveal problems that are difficult to see on an empty product. A bag can look neat on an inspection table and still be frustrating to use if the zipper opening collapses or a divider blocks access to the main compartment.
Szoneier uses material, accessory, pre-production, cutting, sewing, semi-finished, final-product and packaging checkpoints as part of its quality-control approach. The value of these stages is not the number of inspections themselves but the ability to find problems while there is still an efficient opportunity to correct them.
Final Inspection and Tolerances
Final inspection verifies the completed product against the agreed requirements. Typical checks cover overall measurements, appearance, color, stitching, zipper operation, lining, internal pockets, logo quality, hardware finish, surface cleanliness, packaging and SKU identification. The exact inspection criteria should reflect the product type and the retail channel in which it will be sold.
Sewn goods require realistic dimensional tolerances because flexible materials do not behave like injection-molded components. A large soft pouch may naturally show slightly more dimensional movement than a rigid case. Functional dimensions can nevertheless require tighter control. Zipper opening, pocket width and bottle compartment height may matter more to product usability than a small variation in the overall body measurement.
Defects are often considered according to commercial seriousness. A loose thread that can be trimmed before packing is different from a broken zipper, incorrect barcode, missing logo or sharp exposed component. Retail programs may use critical, major and minor defect classifications to separate issues that make the product unsafe or unsellable from minor appearance imperfections.
For larger orders, some customers use AQL-based inspection plans so the sampling size and acceptable defect limits are agreed in advance. The specific AQL level depends on the program, product risk and customer requirements. What matters most is agreeing on the inspection method before production rather than attempting to define acceptable quality only after the goods are finished.
Packaging and Shipment Control
Packaging is part of quality management because correctly sewn products can still arrive damaged, mislabeled or mixed if packing controls are weak. Programs containing several colors, retail labels or distribution destinations require particularly clear SKU allocation and carton instructions.
Individual packaging can range from a simple protective polybag to printed sleeves, paper bands, gift boxes, tissue, insert cards and retail-ready packs. Amazon programs may require FNSKU labels and specific carton markings, while retail distribution centers may use their own barcode and carton-identification standards. These requirements should be reviewed before packaging is ordered because label position or box dimensions can affect the final packing process.
Important packing checks include:
- Correct product and color
- Correct individual package
- Accurate barcode or SKU label
- FNSKU where required
- Correct hangtag or insert
- Correct carton quantity
- Approved carton markings
- Carton dimensions
- Gross and net weight
- Destination labels
- Multi-address shipment allocation
Packaging also affects freight economics. A soft pouch may pack almost flat and allow a high number of units per carton. A structured vanity case placed in a rigid retail box can consume several times more volume even when the actual bag dimensions are similar. Packaging development should therefore consider customer presentation and transportation together rather than treating freight as a problem to solve only after production.
Szoneier can coordinate standard export packing as well as projects involving carton labels, Amazon preparation, split shipments and multi-address delivery. For brands with established warehouse or retail requirements, providing those specifications before sampling allows the product and packaging to be developed as one complete delivery system.
How Do You Choose a Cosmetic Bag Manufacturer?
A suitable cosmetic bag manufacturer should be evaluated through relevant product experience, material knowledge, sampling discipline, production management, quality control, communication and delivery capability. Unit price still matters, but it becomes meaningful only when quotations are based on the same specification. A lower price built on thinner fabric, simpler accessories or different packaging is not genuinely cheaper than another quotation for the intended product.
OEM or ODM
OEM is generally the more appropriate route when a company already has a mature specification. The customer may provide a tech pack, approved physical sample, exact materials, Pantone references, artwork and packaging instructions. The manufacturer’s main responsibilities are then replication, process control, bulk production and maintaining consistency across repeat orders.
ODM becomes more useful when the product direction exists but several manufacturing decisions are still open. A skincare brand may know that it needs a premium travel case for a four-product set but still need help selecting material, establishing dimensions, organizing compartments, choosing reinforcement and determining the most suitable logo process. In this situation, the manufacturer participates more deeply in product development.
| Starting Point | Suitable Route | Typical Factory Role |
|---|---|---|
| Complete tech pack | OEM | Execution and production control |
| Approved physical sample | OEM | Replication and optimization |
| Drawing with partial specification | OEM/ODM | Engineering and sampling |
| Reference images | ODM | Material and structure development |
| Product concept only | ODM | Concept-to-sample development |
| Existing product needing improvement | ODM | Value engineering |
Neither approach eliminates the need for sampling. A detailed OEM specification still needs to be tested using the intended materials and manufacturing process. An ODM project still requires clear written approval once the product has been developed. The practical question is not whether OEM is inherently better than ODM, but how much development work remains between the current idea and a production-ready product.
Supplier Evaluation
A supplier should be evaluated through evidence rather than broad statements such as “professional,” “high quality” or “factory direct.” Start by asking whether the company has made cosmetic bags with similar materials and construction. Experience producing basic polyester zipper pouches does not automatically mean the same team has strong experience with structured PU vanity cases, piping, foam reinforcement and custom hardware.
Sampling processes reveal a great deal about how a factory works. Ask how revision comments are recorded, how approved materials are identified and who is responsible for updating the production standard when a sample changes. A supplier that depends heavily on informal messages can produce a good first sample and still struggle when the product enters repeat manufacturing.
Material knowledge is equally important. A capable manufacturer should be able to explain how polyester, nylon, PU, PVC, TPU, canvas or RPET alternatives will affect structure, printing, cleaning, MOQ and cost. When a factory can only say that every material is “good quality,” the discussion is not yet detailed enough for a serious product decision.
Useful evaluation questions include:
- Have you manufactured similar cosmetic bag structures?
- How are sample revisions documented?
- How are materials approved before production?
- Which logo methods suit the selected fabric?
- How are custom accessories controlled?
- What happens if a material supplier delays delivery?
- Which stages are inspected during production?
- How are repeat-order specifications stored?
- Can several SKUs be produced together?
- How are packaging and shipping requirements checked?
Szoneier works as a factory-based custom bags and soft goods manufacturing partner, supporting material sourcing, sample development, sewing-production coordination, quality inspection, packaging and export delivery. For companies evaluating a new cosmetic bag program, the most useful evidence is not simply a company introduction but whether similar products, materials, samples, quality processes and project records can be reviewed before production begins.
RFQ and Quote Comparison
A detailed request for quotation is one of the simplest ways to improve sourcing accuracy. If three manufacturers receive different information, their prices cannot be compared reliably. One factory may assume basic polyester lining, another may include coated lining, and a third may exclude individual packaging. The resulting quotations can look similar on a spreadsheet while representing different products.
An effective cosmetic bag RFQ should include:
- Reference image, drawing or sample
- Finished dimensions
- Outer material
- Lining material
- Color or Pantone reference
- Structure and compartments
- Reinforcement
- Zipper specification
- Hardware requirements
- Logo method and artwork
- Quantity per color
- Number of SKUs
- Individual packaging
- Retail or barcode requirements
- Destination market
- Required delivery period
- Testing requirements where applicable
If the exact material has not yet been selected, ask suppliers to quote clearly separated alternatives rather than requesting one generic “best price.” Comparing a standard polyester option, a higher-grade nylon alternative and a PU version under the same dimensions and structure can reveal how material affects both price and product positioning.
Quote comparison should also include sample fees, mold or tooling costs, MOQ, component specifications, packaging, production terms and logistics assumptions. A quotation that appears 8% cheaper may stop looking attractive once a weaker zipper, thinner material or excluded retail box is identified. The goal is not to find the smallest number but to determine which manufacturer can deliver the intended product with the fewest uncontrolled assumptions.
Long-Term Production
The value of a good manufacturing relationship increases after the first order because approved patterns, material references, artwork, packaging files and inspection standards no longer need to be rebuilt from zero. A disciplined supplier should retain this information so later replenishment can begin from the most recent approved version rather than from memory or scattered historical messages.
One successful cosmetic bag can also become the foundation for an entire product family. A brand may start with a medium zipper pouch and later develop a smaller gift version, larger travel case, brush organizer, transparent edition or premium PU version. Keeping certain components consistent across the collection can simplify sourcing while allowing the visible product range to expand.
Common elements that can sometimes be shared include zipper specifications, lining families, hardware finishes, logo dimensions and packaging formats. Standardization does not mean making every SKU identical. It means adding complexity where customers can see or use it while avoiding unnecessary unique components in areas that do not create meaningful value.
This is particularly useful for companies building repeat programs. Stable records of materials, patterns, approved samples and production changes make it easier to evaluate substitute components if something becomes unavailable. They also give the manufacturer a much stronger reference point when an order is repeated six or twelve months later.
Conclusion
A successful custom cosmetic bag is rarely the result of one dramatic manufacturing decision. It comes from dozens of smaller choices that work together: selecting a material that fits the brand position, creating an opening that customers can actually use, choosing branding that performs on the selected surface, approving measurable sample revisions, controlling components before sewing, inspecting production while corrections are still practical and developing packaging that reaches the final destination efficiently.
The strongest projects also avoid treating cost, MOQ, quality and design as separate conversations. A custom zipper changes cost and MOQ. A thicker lining can change sewing behavior. More colors can change material purchasing. A rigid gift box can change freight volume. Once those relationships are understood, quotations become easier to compare and product development becomes far more predictable.
Szoneier approaches custom cosmetic bags as part of a wider custom bags and soft goods manufacturing system, supporting product development from material and structural decisions through sampling, bulk production, quality inspection, packaging and delivery. For brands planning a first cosmetic pouch or expanding an existing beauty-accessory range, the most productive starting point is a clear product brief and a realistic discussion about what the finished product needs to achieve. When those fundamentals are defined early, the approved sample has a much better chance of becoming the same product customers eventually receive.
Frequently Asked Questions
What Is the MOQ for Custom Cosmetic Bags?
The MOQ depends on the outer material, lining, number of colors, logo process, accessories, packaging and structure rather than on one universal factory number. Szoneier supports selected standard cosmetic bag projects from approximately 200 pieces when available fabrics, regular colors and common accessories are suitable. Projects requiring custom-dyed materials, molded hardware, special packaging or unusual certified components may need higher quantities because individual component suppliers can impose their own minimum purchasing requirements.
How Long Does It Take to Manufacture Custom Cosmetic Bags?
Manufacturing time should be viewed as several stages rather than one fixed number. A project normally includes requirement confirmation, material sourcing, sample development, revision, final approval, bulk material preparation, cutting, sewing, inspection and packaging. Simple bags using available materials and standard accessories generally move more quickly than structured products requiring custom colors, molded zipper pullers or printed retail boxes. Shipping and customs time should also be added separately when planning the retail launch date.
Which Material Is Best for a Custom Makeup Bag?
Polyester is a practical choice for many everyday and promotional bags because it offers broad color and printing options, while nylon can provide a smoother and more technical appearance. PU works well for fashion-oriented and premium products, canvas creates a natural textile look, and PVC or TPU can be useful for transparent or wipe-clean designs. The best material depends on the intended use, target price, cleaning requirements, brand positioning and construction rather than on one material being universally superior.
Can Custom Cosmetic Bags Be Made Waterproof?
Cosmetic bags can be made more water-resistant through coated fabrics, TPU, PVC, waterproof-style zippers and specialized seam construction, but a water-resistant fabric does not automatically make the finished bag completely waterproof. Needle holes, zipper openings and sewn seams can still allow moisture through. If waterproof performance is commercially important, the construction should be specifically engineered for that purpose and the required performance should be defined through an appropriate test rather than relying only on the material description.
What Logo Methods Work Best on Cosmetic Bags?
The appropriate branding method depends on the material and artwork. Screen printing and heat transfer work well for many textile pouches, embroidery creates texture on suitable fabrics, woven labels provide consistent branding across different materials, and debossing or hot stamping can work well on selected PU surfaces. Metal plates, rubber patches, silicone patches and custom zipper pullers offer additional options. Logo size, detail, durability, MOQ and production stability should all be reviewed during sampling before bulk components are ordered.
What Should I Send a Manufacturer for an Accurate Quote?
An accurate quotation should begin with a reference image, drawing, tech pack or physical sample together with finished dimensions, preferred outer material, lining, color, logo artwork, zipper requirements, internal compartments, order quantity, color breakdown, packaging expectations, destination country and desired delivery period. If some specifications are still undecided, say so clearly and request defined alternatives. Providing complete information allows different factory quotations to be compared on the same basis rather than on hidden assumptions.
How Can I Keep Bulk Production Consistent With the Approved Sample?
Consistency improves when the approved sample is supported by written specifications rather than being used as the only reference. Record critical dimensions, materials, colors, zipper and hardware specifications, logo size and position, packaging requirements and any approved sample revisions. Quality checks should then take place before and during production as well as at final inspection. This makes it possible to identify material or sewing deviations early instead of discovering them only after the entire order has been completed.