Skip to content

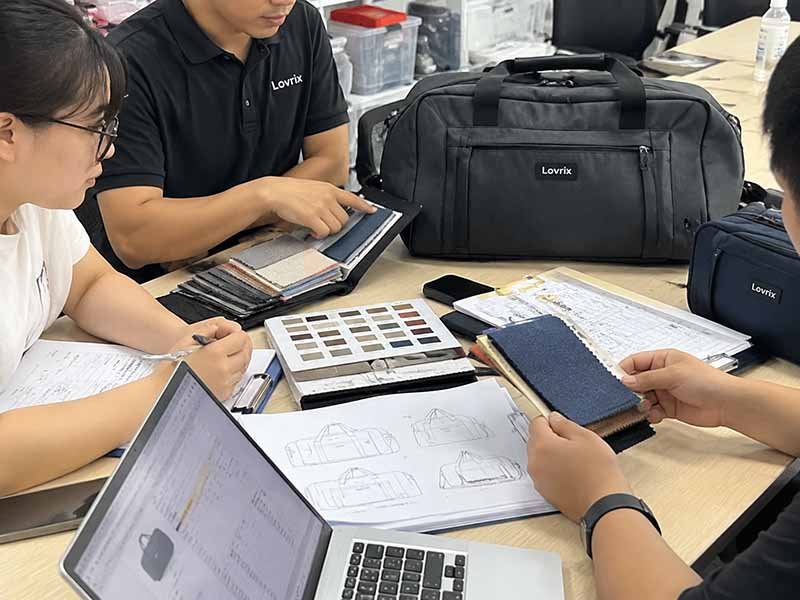
Choosing a bag manufacturer for a retail program is very different from finding a factory that can make one attractive sample. A retail program may start with one style, but it can quickly expand into several colors, multiple SKUs, custom packaging, retailer labels, repeated purchase orders, seasonal replenishment, and tighter delivery windows. The first sample may look perfect, yet the real manufacturing challenge begins when that same product has to be reproduced thousands of times without losing its shape, color, workmanship, packaging accuracy, or commercial viability.
The right manufacturing partner should therefore be judged as a complete operating system rather than as a sewing workshop. Product development, material sourcing, sampling, production control, quality inspection, packaging, compliance coordination, shipment preparation, and reorder documentation all need to work together. A low quotation can be attractive at the beginning, but inconsistent production, unclear specifications, barcode errors, late material arrivals, or uncontrolled substitutions can cost far more once the goods are tied to a fixed retail launch.
A useful way to think about the decision is simple: the first order proves that a factory can make the product once, while the next several orders prove whether the factory can support the program. The strongest manufacturer is not necessarily the one with the largest building, the lowest MOQ, or the cheapest unit price. It is the one that can turn your approved product into a repeatable production standard and keep that standard stable as volume, colors, packaging, and replenishment requirements become more complicated.
What Makes a Bag Manufacturer Fit for Retail Programs?

A bag manufacturer is suitable for retail programs when it can control product development, materials, bulk production, quality, packaging, delivery, and repeat orders as one connected process. Retail projects require more than sewing capacity because every approved detail must remain consistent across different SKUs, production batches, and replenishment orders. A capable factory should be able to explain how those standards are documented, checked, and reproduced.
Category Experience Matters
Relevant experience should be judged by manufacturing difficulty, not simply by whether the factory has made something that looks similar. A supplier that specializes in basic promotional tote bags may produce large quantities very efficiently, but that does not automatically make it suitable for a technical backpack with padded compartments, several zipper types, reinforced webbing, custom hardware, embroidery, retail labels, and strict appearance standards. The processes, failure points, and production controls are completely different.
A stronger evaluation compares the actual manufacturing problems behind the product. Look at the material family, number of components, sewing complexity, reinforcement requirements, hardware, logo method, finishing quality, retail packaging, and expected order size. If a company is developing a cosmetic bag, experience with lining, piping, zipper installation, surface cleanliness, logo positioning, and compact retail packaging may be more valuable than experience with unrelated bags that only share a similar outer shape.
Experienced manufacturers also tend to ask more useful questions before quotation. A factory familiar with backpacks will usually notice shoulder-strap reinforcement, bartacks, laptop compartment dimensions, zipper stress points, and pocket usability. A factory experienced with cooler bags will pay attention to insulation thickness, lining construction, seam treatment, odor, closure, and leakage risks. When the questions are specific, practical, and connected to the product’s real use, they are often a better indicator of expertise than a large product gallery.
Look Beyond the Factory Label
Companies often begin supplier qualification by asking whether the business is a factory or a trading company, but the label by itself does not answer the most important question: who actually controls the project? A factory may still be poorly organized if sales, sampling, purchasing, production, and inspection operate independently. On the other hand, a well-managed manufacturing organization may coordinate several specialized production resources while keeping one controlled set of standards and one accountable project team.
The practical issue is how many uncontrolled handoffs sit between your approved specification and the production floor. Ask who develops the sample, who controls the pattern, who purchases materials, who approves substitutions, who manages production documents, who inspects early production, and who has authority to stop work when something is clearly wrong. A retail program becomes risky when nobody can answer those questions clearly or when responsibility constantly moves from one department to another.
Video reviews and factory visits are useful because they reveal how the operation actually works. A serious review should cover the sample area, material storage, cutting, sewing, semi-finished goods, inspection, packing, and examples of similar products. The objective is not to inspect a factory as if every workstation needs to look perfect. It is to understand whether product information moves through the business in a controlled way and whether the same standards are visible from development through shipment.
Ask for Evidence, Not Claims
Most suppliers use similar language: professional service, good quality, competitive price, fast delivery, and many years of experience. Those statements are difficult to evaluate because they are not specific enough to influence a serious sourcing decision. A stronger approach is to convert each important claim into something that can be reviewed, measured, or verified before a meaningful order is placed.
| Supplier Claim | Useful Evidence | What It Helps Confirm |
|---|---|---|
| “We make this type of bag” | Similar samples, project photos, production records | Category experience |
| “We control quality” | QC checkpoints, inspection sheets, defect examples | Process discipline |
| “We support retail programs” | Hangtags, barcode labels, carton marks, assortment examples | Retail readiness |
| “We can handle volume” | Production plan, line allocation, capacity explanation | Capacity realism |
| “We can repeat the product” | BOM, patterns, material references, approved sample records | Reorder consistency |
| “We support compliance” | Valid reports, audit documents, testing process | Compliance capability |
| “We manage many SKUs” | SKU matrix, revision tracking, packing matrix | Program control |
Pay attention to how a manufacturer responds when proof is not immediately available. A responsible answer may be, “That report does not currently cover this material, but we can arrange the appropriate test for your target market.” That type of answer is often more useful than an unconditional statement that the product is already compliant everywhere. A mature manufacturing partner should be comfortable distinguishing what has already been verified from what still needs to be confirmed.
For retail programs, evidence should gradually form a chain. Comparable products show category experience, sample records show development control, specifications show repeatability, inspection records show quality discipline, packaging samples show retail readiness, and reorder documentation shows whether the supplier can support future business. The stronger that chain becomes, the less the sourcing decision depends on sales language or first impressions.
How Do You Evaluate Product Development and Sampling?

Product development and sampling should be evaluated as a controlled translation process from idea to production standard. A capable manufacturer should clarify requirements, identify technical risks, confirm materials and components, record revisions, and establish one final approved reference before bulk production begins. The goal is not merely to produce a good-looking prototype, but to create a product that can be repeated commercially without constant reinterpretation.
Start With a Complete Product Brief
Sampling problems often begin long before the first piece of fabric is cut. When a factory receives only one reference image and a target price, many important details have to be guessed. The supplier may need to assume the fabric weight, lining, zipper quality, foam thickness, internal structure, hardware, reinforcement, logo process, and even the level of finishing expected. Those assumptions may produce a sample that looks acceptable in photographs but does not match the intended product strategy.
A useful product brief should include the product dimensions, intended use, material direction, lining, major pockets, key accessories, logo artwork, colors, quantity, number of SKUs, packaging, destination market, target cost range, and desired delivery schedule. If a tech pack already exists, it should be shared early. If a physical reference sample is available, explain which elements should remain unchanged and which ones are meant to be improved, simplified, upgraded, or reduced in cost.
This early clarification is especially important when several objectives compete with one another. A thick canvas, heavy foam, premium zipper, custom metal logo plate, rigid box, and low target price may not work together commercially. Product development should expose those conflicts before money is committed to tooling, materials, or mass production. A strong manufacturer does not simply follow instructions; it helps turn broad preferences into a set of decisions that can actually be manufactured at the required quality and cost.
Control Materials Before You Control the Bag
Many visible differences between sample and bulk production begin with materials rather than sewing. Terms such as nylon, polyester, Oxford, canvas, PU, or leather are broad categories, not precise specifications. Two fabrics sold under the same general name may differ in weight, weave, coating, backing, texture, gloss, softness, color behavior, abrasion performance, and water resistance. Similar differences apply to zippers, sliders, buckles, webbing, foam, lining, thread, metal parts, patches, and printed materials.
Important components should therefore have an approval reference. Depending on the project, this may include a supplier material code, physical swatch, Pantone reference, approved zipper sample, buckle sample, webbing specification, foam thickness, printed logo proof, embroidery sample, woven-label proof, or packaging artwork. The objective is not to create unnecessary paperwork, but to eliminate ambiguity around the parts that affect appearance, performance, cost, and consistency.
Color-sensitive retail programs need particular care. A digital color reference is useful for communication, but a physical swatch or approved lab dip is more reliable when color is important to the collection. If several SKUs share the same fabric, sourcing them from one controlled lot may improve consistency. When the product will be reordered months later, material references become even more important because a new production lot can vary slightly even when the commercial specification remains unchanged.
The best material-control systems also define what happens when something is unavailable. A component should not simply be replaced with a “similar” alternative during production. The manufacturer should identify the issue, propose an alternative, explain appearance or performance differences, show any cost or lead-time impact, and obtain approval before changing the specification. That process protects the product from quiet substitutions that may seem minor at the factory but become obvious on the retail shelf.
Manage Samples Like Versions
Sample revisions become confusing when feedback is spread across emails, chat messages, photos, comments, and phone calls. A cleaner approach is to treat each sample as a controlled version. Sample V1 may establish the initial construction, V2 may correct the handle length, V3 may adjust the logo position, and V4 may confirm final materials and packaging. When the product is finally approved, one version should clearly become the production reference.
Each meaningful change should identify what was modified and whether the change affects price, materials, tooling, or lead time. Suppose a second sample corrects the strap length but accidentally uses the old zipper, while a third sample fixes the zipper but changes the logo placement. If different team members approve different details from different samples, production can begin without one complete approved standard. Version control prevents that situation from becoming a dispute later.
Before bulk production starts, the project should be able to answer several questions without hesitation. Which sample is final? Which measurements are approved? Which fabrics and accessories are approved? Which logo file is final? Which packaging artwork is final? Which changes have been rejected? Which details are still open? The more clearly these questions are answered before production, the less interpretation remains for sewing lines, packing teams, and inspectors.
A good final sample is therefore more than a prototype. It becomes a physical manufacturing standard supported by written specifications. For more complicated retail programs, a pre-production sample made with production materials can provide one additional checkpoint before large quantities are released. That step is especially useful when materials, hardware, or packaging have changed since the last development sample.
How Do You Control Sample-to-Bulk Consistency?

Sample-to-bulk consistency is controlled by converting the approved sample into a repeatable production system. Materials, dimensions, accessories, logo files, workmanship requirements, packaging instructions, and inspection points should be locked before bulk production. Quality should then be checked at several stages while goods are being produced, so recurring problems can be corrected before thousands of units have already passed through the same process.
Build a Production Control Pack
An approved physical sample is important, but it should not be the only source of truth. Samples show appearance very well, yet they may not reveal hidden information such as foam thickness, coating details, zipper specification, fabric code, internal reinforcement, thread type, tolerances, or the exact packaging arrangement. Those details need to be recorded separately if the product is expected to be reproduced reliably.
A practical production control pack usually includes the final approved sample, measurement sheet, BOM, pattern reference, approved material information, accessory specifications, logo artwork, packaging instructions, and quality requirements. A simple cotton tote may need only a small amount of documentation, while a travel backpack with multiple compartments and custom hardware requires a much more detailed set of references. The level of documentation should follow product complexity and commercial risk.
Critical measurements deserve special treatment. Sewn products naturally have variation, so it is not useful to impose extremely tight tolerances on every dimension. Instead, identify the measurements that influence fit, function, appearance, or compatibility. For a laptop backpack, this may include laptop sleeve size, opening width, shoulder-strap length, trolley sleeve width, and finished body dimensions. For a cosmetic pouch, zipper opening, overall shape, logo position, and internal divider dimensions may matter more.
When those specifications are clear, the production team has fewer decisions to make on its own. The control pack becomes a common reference for sourcing, cutting, sewing, inspection, packing, and later replenishment. That common reference is one of the most effective ways to reduce the familiar problem where a beautiful development sample gradually becomes a slightly different product by the time the full order is complete.
Manage Material and Component Changes
Retail programs may run for several seasons, but materials and components do not always remain available forever. Fabric mills change lots, zipper suppliers discontinue pullers, hardware finishes shift, coatings are reformulated, and packaging materials are updated. Even when a component still carries the same commercial description, the actual appearance or performance can vary from the version used in an earlier order.
A controlled change process should therefore be part of the manufacturing relationship. When a component becomes unavailable, the supplier should identify the issue, provide an alternative, compare the relevant specifications, explain visual or functional differences, state any cost or delivery impact, and obtain approval before production continues. The objective is not to prevent all change, because some change is unavoidable, but to make sure changes are visible and authorized.
Shared components across several SKUs also need centralized control. If three styles use the same zipper pull but one production line substitutes a different finish, the individual units may still function correctly while the collection loses visual consistency. The same problem can occur with webbing colors, lining shades, print inks, hardware plating, or packaging paper. A retail program should therefore be reviewed as a connected product family rather than as a group of unrelated orders.
Physical references remain useful in this process. An approved swatch, zipper sample, hardware piece, or packaging sample often communicates subtle details more effectively than text alone. When the program is likely to repeat, storing these references alongside digital records can make future orders easier to verify. The goal is to preserve enough information that the product can survive supplier changes, staff turnover, and long gaps between orders without having to be reinvented.
Inspect Quality During Production
Final inspection is essential, but it happens late. If a repeated sewing defect is discovered only after all units have been completed, the factory may face extensive rework, delayed packing, or a difficult negotiation over acceptance. Quality becomes more effective when checks are placed earlier in the process, especially at points where one mistake can spread quickly across the entire order.
| QC Stage | Typical Checks | Main Purpose |
|---|---|---|
| Incoming materials | Color, fabric defects, coating, accessories | Prevent poor inputs entering production |
| Pre-production | Sample, BOM, artwork, packaging | Confirm the production standard |
| Cutting | Measurements, direction, matching | Catch pattern or cutting errors |
| Sewing | Stitching, alignment, reinforcement, assembly | Detect repeat defects early |
| Semi-finished | Structure, pockets, zippers, shape | Confirm assembly before finishing |
| Final inspection | Appearance, dimensions, function | Verify finished product quality |
| Packing | SKU, barcode, hangtag, carton quantity | Protect retail and logistics accuracy |
Inspection priorities should change with the product. A backpack may require special attention to shoulder attachments, bartacks, zipper operation, laptop compartment dimensions, and load-bearing areas. A cooler bag may need closer control of the lining, insulation, seam construction, zipper closure, and odor. A cosmetic bag may place more emphasis on surface appearance, logo placement, lining cleanliness, zipper smoothness, and finished shape.
The key question is not simply whether a factory “has QC.” A more useful question is what inspectors check at each stage, which reference they use, what defect limits apply, and what happens when a recurring problem appears. A quality system is valuable when it changes production behavior, not when it exists only as a checklist completed at the end of the order.
Which Retail-Ready Requirements Should the Factory Manage?

A retail-ready manufacturer should manage the product together with the information and packaging needed for the sales channel. Hangtags, barcodes, warning labels, individual packaging, carton quantities, carton marks, assortment packing, inserts, retailer protocols, and shipment documents may all be part of the finished program. A correct bag can still become an operational problem if the wrong SKU, label, or packing configuration reaches the warehouse.
Build Packaging Around the Sales Channel
Packaging should be developed around how the product will be sold, handled, shipped, and presented. A premium lifestyle store may value a dust bag, branded tissue, hangtag, and elegant box, while a warehouse retailer may prefer packaging that is simple, durable, easy to scan, and efficient to replenish. An e-commerce brand may want a strong unboxing experience but still needs to avoid excessive parcel dimensions and unnecessary shipping weight.
Protection is the first consideration, but it is not the only one. Packaging may also need to support barcode visibility, shelf display, hanging presentation, sustainability targets, warning labels, internal SKU identification, and efficient carton packing. A packaging decision that adds only a small amount per unit can still become financially meaningful at retail-program scale. An extra $0.30 per unit across 30,000 pieces adds $9,000 before any effect on carton dimensions or freight is considered.
Carton efficiency deserves attention because a visually attractive retail box can increase shipping volume. If changing the packaging reduces the number of units that fit in a master carton, transport cost can rise even when the packaging material itself is inexpensive. For that reason, packaging should be reviewed together with product dimensions, carton quantity, pallet or container use, and the actual requirements of the sales channel.
It is also useful to separate customer-facing packaging from logistics packaging. The retail unit may use a branded sleeve or hangtag, while the shipment still requires inner packs, master cartons, carton marks, handling symbols, and destination labels. When these layers are planned together, the product can move from factory to warehouse to store with fewer manual corrections along the way.
Control SKU and Barcode Accuracy
SKU accuracy becomes increasingly important as a collection expands. A program with four styles and three colors already contains twelve SKUs. At 2,000 units per SKU, that creates 24,000 individual products that must be matched correctly with their color, internal style number, hangtag, barcode, polybag label, carton allocation, and shipment documentation.
The safest way to manage this complexity is with one controlled SKU matrix. It should connect the customer’s SKU, the factory style number, color, size, barcode, artwork, unit packaging, carton quantity, carton mark, and order quantity. The first packed units from each SKU should be checked against this reference before the entire order is packed, because correcting a mistake after thousands of labels have been attached is much more expensive.
Barcode execution should also be tested, not only reviewed visually. A code can look correct to the eye but still create scan problems because of poor print quality, scaling, contrast, damaged quiet zones, or incorrect encoded data. Actual printed labels should be scanned before mass packing begins. Retail operations depend on accurate identification, and a barcode problem can affect receiving, inventory, replenishment, and checkout long after the product has left the factory.
Version control is just as important for packaging files as it is for samples. Files named “final,” “final-new,” or “final-2” often cause confusion when several people are involved. A stronger process uses clear version numbers, approval dates, and SKU references. Small improvements in file discipline can prevent surprisingly large operational mistakes when a program includes many products with similar artwork.
Confirm Compliance Before Production
Compliance should be discussed during product development because testing can influence material selection, component choice, construction, labeling, and lead time. An adult tote bag, children’s backpack, insulated lunch bag, medical pouch, or functional protective bag may face very different requirements. The relevant standard depends on the product, market, age group, materials, claims, and sales channel rather than on the fact that everything falls broadly under the category of bags.
Before arranging tests, the project should identify the country of sale, retail channel, intended user, material composition, metal components, coatings, food-contact considerations, performance claims, and any retailer-specific protocol. Large retail organizations may add requirements beyond basic national regulations, including chemical restrictions, label rules, packaging standards, inspection procedures, or social-responsibility audits. Those requirements should be collected early enough to affect development decisions.
One common mistake is assuming that a factory certificate automatically proves every product is compliant. Another is assuming that a report on one material or color applies to every variation. Test reports have a defined scope, and changing materials, components, colors, or suppliers may affect whether the previous result still applies. The relevant document should always be reviewed for the tested sample, standard, date, holder, and intended use.
A responsible manufacturer should clearly separate existing documentation from tests that need to be arranged for a specific project. That approach may feel less impressive than claiming that every product is already certified, but it is much safer for a serious retail program. Compliance works best when it becomes part of product planning rather than a paperwork exercise performed immediately before shipment.
How Do You Evaluate MOQ, Capacity, Cost, and Lead Time?
MOQ, capacity, cost, and lead time should be evaluated together because changing one often changes the others. More colors can increase material minimums, custom hardware can extend procurement time, small quantities can raise setup cost, and complex packaging can reduce daily output. A meaningful quotation should therefore explain the assumptions behind the price and show how the manufacturing schedule connects to materials, production, inspection, and packing.
Understand the Real MOQ
A single MOQ number rarely tells the whole story. If a factory says the minimum order is 500 pieces, the next question is whether that means 500 pieces total, 500 per style, 500 per color, or 500 per material. The factory may be willing to sew a smaller quantity, while the material mill, zipper supplier, hardware manufacturer, or packaging printer requires a higher minimum for custom production.
Custom-dyed fabrics, special zipper colors, woven webbing, molded hardware, printed lining, and branded retail packaging can each create their own minimum quantities. A project may therefore have several layers of MOQ operating at the same time. The finished product MOQ could be relatively flexible, while one component forces the total quantity higher or requires excess material to be purchased.
The most useful supplier conversation separates these layers. Ask what minimum applies to the finished product, the main material, special accessories, and custom packaging. If several colors are planned, ask whether the material minimum applies per color. If several styles share the same fabric or hardware, ask whether quantities can be combined to reach supplier minimums. Those details can significantly improve assortment planning.
Low MOQ can be helpful for new products, but it should not be treated as automatically better. Very small runs often carry higher unit cost, more material limitations, fewer custom-component options, and less production efficiency. The right MOQ is the quantity that balances commercial risk with a specification that still represents the intended product.
Compare Like With Like
Unit prices should never be compared until specifications are normalized. One supplier may quote a lower price because it uses lighter fabric, simpler zippers, thinner foam, generic hardware, basic packaging, or a different incoterm. Another may include components and services that appear more expensive at first but reduce later work. Without aligning those assumptions, the lowest quotation may simply represent a different product.
A useful comparison should cover material construction, lining, foam, zippers, hardware, webbing, reinforcement, logo method, packaging, inspection, testing, quantity, and shipping terms. One-time charges such as tooling, molds, screens, samples, testing, and setup should be separated from the unit price so the effect on first orders and later reorders can be understood more clearly.
Specific quotations are easier to manage than broad ones. “$8.20 per unit” says very little. “$8.20 per unit for 3,000 pieces using the approved polyester specification, selected lining, agreed zipper, embroidered logo, individual polybag, and FOB shipping term” provides a commercial reference that can be compared. If the target cost needs to fall, the team can then discuss which specification changes are acceptable rather than simply asking the supplier to reduce the price.
Cost should also be evaluated against variation risk. Saving $0.25 per unit on 20,000 pieces saves $5,000, but that saving becomes less attractive if packaging errors, high defect rates, late delivery, or inconsistent materials create rework and retailer penalties. A retail program benefits from competitive pricing, but the real objective is predictable landed cost and fewer expensive surprises.
Test Capacity Against Your Timeline
Published monthly capacity can be misleading because simple and complex products consume production resources differently. A sewing line that can produce a large number of basic drawstring bags cannot necessarily produce the same quantity of technical backpacks. Material preparation, operator skill, number of operations, equipment, inspection, and packaging all influence the actual output for a specific program.
Instead of asking only for monthly capacity, ask how much relevant capacity is available during the exact production window your project needs. The factory should be able to explain when materials will arrive, when the pre-production standard will be confirmed, when cutting starts, how sewing is scheduled, when in-line inspection occurs, when packing begins, and when the goods are expected to become cargo-ready.
As a practical planning reference, relatively simple sewn bags may often require around 20–30 days for bulk production once materials and approvals are ready, while more complex bags can require approximately 40–60 days or longer. Sample development may take several working days for straightforward products and longer when structure, custom materials, or repeated revisions are involved. These ranges are planning references rather than guarantees because every project has different constraints.
Peak season needs additional attention. If a retail launch cannot move, the schedule should not be built around the best possible scenario. Material delays, sample revisions, production congestion, testing, inspection, and shipping can all consume time. A modest schedule buffer is often cheaper than emergency air freight or a missed launch, particularly when several SKUs need to arrive together.
How Do You Assess Reorders and Long-Term Support?
Long-term support is measured by whether the factory can reproduce the approved product without rebuilding the project from memory. Strong reorder management keeps patterns, BOMs, material references, accessory specifications, artwork, packaging files, quality standards, and revision history under control. As a retail program grows, those records make replenishment faster, reduce repeated development work, and help prevent small specification changes from becoming permanent inconsistencies.
Protect the Product Record
A reorder should begin with a controlled product record rather than an old email saying, “Please make exactly the same as last time.” People change, material suppliers change, factories become busy, and several months may pass between production runs. Without reliable documentation, the original product gradually depends on memory, which is one of the weakest forms of manufacturing control.
For a repeat product, retain the final pattern, measurement sheet, BOM, material references, zipper specification, hardware references, logo files, packaging files, approved sample information, quality requirements, and revision history. When the next purchase order begins, those records should be reviewed together so the team can identify which items are unchanged and which need to be reconfirmed.
Material continuity deserves particular attention. A custom navy fabric produced ten months earlier may not match a new lot perfectly, even if it carries the same material code. The correct process is to compare the new material with the approved reference and flag any meaningful difference before production begins. The same principle applies to coatings, leather grain, hardware finish, zipper tape, webbing, lining, and printed materials.
Repeatability does not mean that nothing ever changes. It means changes are controlled, visible, and approved. A mature manufacturing relationship gets stronger over time because each order leaves behind better records. The second order should require less uncertainty than the first, and the fifth order should be easier to manage than the second.
Manage SKU Growth Before It Becomes Chaos
Retail programs often become more complex after they become successful. A company may start with two styles in two colors, which creates only four SKUs. One year later, the same line may include more colors, a smaller size, a premium version, different packaging for another market, and several replenishment orders running at once. The complexity can grow much faster than the total volume.
A SKU master provides one reference point for that expansion. It should connect customer SKU, factory style number, version, color, material, logo, barcode, packaging, carton quantity, approval status, and production status. Version numbers are particularly important when a product changes. If a zipper, compartment, or package is updated, the previous version should remain identifiable rather than being overwritten.
| Control Field | Example |
|---|---|
| Customer SKU | BP-104-NVY |
| Factory Style | SZ-BP104 |
| Product Version | V2 |
| Color | Navy |
| Main Material | 600D Polyester |
| Logo Method | Embroidery |
| Barcode | SKU-specific file |
| Unit Packaging | Hangtag + PE bag |
| Carton Pack | 20 pcs/carton |
| Status | Approved / Production / Reorder |
This type of control becomes even more important when production is distributed across several sewing lines or specialized partner facilities. Flexible capacity can be valuable, but only when the product standard remains centralized. The production location may change, while the approved sample, BOM, materials, packaging instructions, inspection requirements, and project responsibility should remain consistent.
Choose for the Next Order, Not Only the First
The first purchase order often receives the most attention because both sides are trying to establish the relationship. The more revealing test comes later, when the product becomes routine. A useful manufacturing partner should still perform well when the order doubles, new colors are added, a component becomes unavailable, retail packaging changes, replenishment becomes urgent, or several seasonal launches overlap.
Before choosing a long-term manufacturer, discuss those situations directly. Ask how the team handles discontinued materials, urgent reorders, repeated quality problems, expanding SKU counts, seasonal capacity pressure, and specification changes. The answers do not need to be perfect, but they should show a clear operating process rather than improvisation.
One practical way to structure a supplier decision is to consider product capability, development, quality control, retail packaging, compliance support, cost, capacity, communication, and reorder systems together. The weighting should match the program. A premium brand may place more emphasis on material and workmanship consistency, while a high-volume retail program may give more weight to production capacity, cost discipline, and on-time delivery. Products with stronger regulatory requirements may treat compliance as a pass-or-fail condition rather than merely another scoring category.
The best long-term relationship is one in which the factory gradually reduces the amount of uncertainty the retail team has to manage. Samples become easier to approve, recurring materials are better documented, quotations become clearer, quality history becomes visible, and reorders need less explanation. That is the point where a manufacturer stops functioning as a one-order supplier and begins supporting the program as part of a stable supply chain.
A reliable bag manufacturer for retail programs should therefore be evaluated across the complete life of the product, not only during the first quotation. The strongest suppliers combine category knowledge, disciplined product development, controlled materials, repeatable production, practical quality inspection, retail-ready packaging, realistic capacity, and organized reorder records. These capabilities help protect the product when the program expands from one style into several SKUs, larger volumes, new markets, and repeated seasonal orders.
The final decision should feel less like choosing the cheapest factory and more like choosing the operating system behind the product. When specifications are clear, changes are controlled, quality is checked early, packaging is accurate, and reorder information is preserved, both sides spend less time correcting avoidable mistakes. That creates a much healthier foundation for retail growth because the manufacturing process becomes increasingly predictable instead of becoming more difficult every time the program gets larger.
Frequently Asked Questions
What should I check first when choosing a bag manufacturer for a retail program?
Start with product-category fit, development capability, material control, quality process, retail packaging, and repeat-order systems rather than unit price alone. Ask for evidence of similar products and review how the factory moves from sample approval to bulk production. A manufacturer that can explain specifications, production checkpoints, packaging control, and future replenishment usually provides a stronger foundation than one that focuses mainly on low price or general claims about quality.
How many samples should be made before bulk production?
There is no fixed number because product complexity and development quality vary. A simple tote bag may reach approval after one or two rounds, while a structured backpack, cooler bag, or multi-material product may require several revisions. The important point is not the number of samples but whether each revision closes clearly documented issues. Bulk production should begin only when materials, dimensions, components, logo execution, workmanship, and packaging have a final approved reference.
What is a reasonable MOQ for custom retail bags?
MOQ varies significantly by product structure, material, colors, accessories, logo process, and packaging. Some straightforward custom bags may begin at a few hundred pieces, while custom-dyed fabrics, molded hardware, proprietary zipper colors, or printed retail packaging can push minimums much higher. Always ask whether the quoted MOQ applies to the total order, each style, each color, or a specific material so assortment planning is based on the real production constraints.
How can I prevent bulk bags from looking different from the approved sample?
Use the approved sample together with a written production control pack that includes measurements, BOM, material references, accessory specifications, logo files, packaging instructions, and quality checkpoints. Important materials and components should be approved before production, and substitutions should require authorization. In-process inspections are also important because recurring defects are easier to correct while production is still running than after every unit has been completed.
What packaging details should be confirmed for retail orders?
Confirm unit packaging, hangtags, barcode files, labels, warning information, inserts, carton quantity, carton marks, assortment packing, and any retailer-specific requirements before bulk packing begins. For collections with several SKUs, use a packaging matrix that links each SKU to its correct barcode and carton configuration. Actual printed barcodes should also be scanned before full packing, because a label that looks visually correct can still create problems during receiving or checkout.
How early should a retail program start production before the launch date?
The schedule should be planned backward from the required warehouse or store date rather than from the factory’s quoted production time alone. Allow time for sample approval, material preparation, production, inspection, packing, testing if required, and transportation. Simple bags may move through production faster than technical or highly customized products, and peak-season congestion can add further risk. Programs with fixed launch dates should include buffer rather than relying on a best-case timeline.
What makes a manufacturer suitable for long-term replenishment orders?
Long-term replenishment depends on documentation and control. The manufacturer should retain the approved pattern, BOM, material and accessory references, logo files, packaging files, quality standards, and revision history. It should also have a clear process for handling unavailable materials, new production lots, changing SKUs, and urgent reorders. The real test is whether each repeat order becomes easier and more predictable instead of requiring the product to be redeveloped from the beginning.