Skip to content

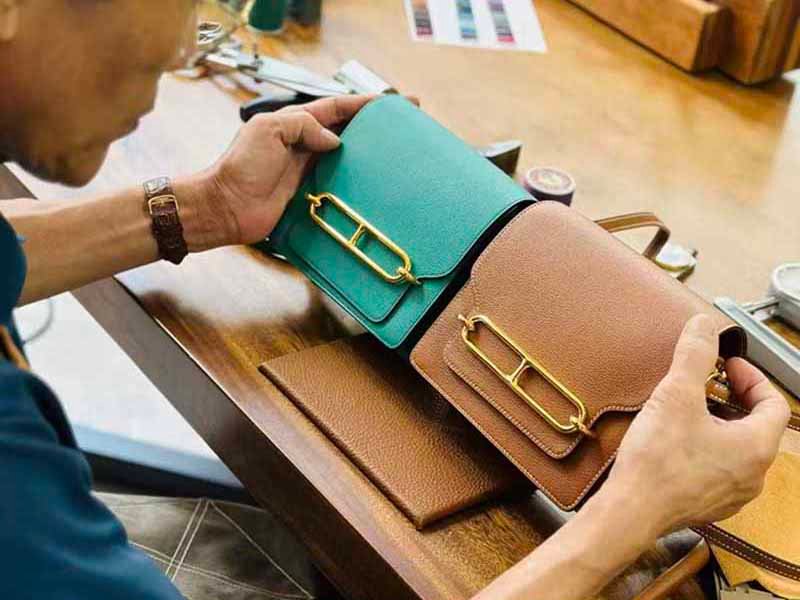
A finished leather bag can look deceptively simple. The customer sees leather, handles, a zipper, lining, hardware, perhaps a metal logo, and a clean silhouette. A manufacturer sees something very different: leather grade, usable cutting yield, thickness, skiving zones, reinforcement, seam allowances, zipper construction, hardware anchoring, edge finishing, pattern tolerances, production sequence, inspection points, packaging pressure, and dozens of decisions that determine whether the same product can be reproduced consistently across hundreds or thousands of pieces.
Custom leather bags are manufactured by turning a product concept into controlled specifications, developing and approving a physical sample, confirming leather and components, preparing patterns, cutting and skiving leather, reinforcing stress areas, sewing and assembling components, finishing edges, inspecting production, and packing the approved product for shipment. The real objective is not making one attractive sample, but building a repeatable production standard that remains consistent in bulk.
This distinction becomes important as soon as a project moves beyond the prototype. A sample maker can spend extra time adjusting one piece until it looks excellent, but commercial manufacturing has to repeat the same dimensions, grain direction, edge quality, hardware placement, stitching, structure, and color across an entire order. When brands receive bulk goods that feel different from the sample, the problem often began much earlier than final inspection. A leather specification may have been too vague, a reinforcement detail may have remained undocumented, or the approved hardware may never have been converted into a controlled production standard.
For brands developing a leather tote, handbag, crossbody bag, backpack, business bag, pouch, or other leather goods, understanding the manufacturing process is therefore less about learning how to sew and more about learning how design decisions become repeatable production decisions. Szoneier approaches custom bag projects through material selection, structure development, pattern making, sampling, production coordination, quality inspection, packaging, and export delivery rather than treating sewing as an isolated factory operation. The sections below explain what should happen at each stage and where the most expensive mistakes can usually be prevented.
What Do You Need Before Manufacturing a Leather Bag?

Before manufacturing begins, define the bag type, target dimensions, intended use, material direction, construction, hardware, branding, order quantity, packaging, and destination market. You do not need a perfect technical package at the first conversation, but every important design decision should eventually become a measurable specification before bulk production starts, otherwise different people may interpret the same product in different ways.
Start With a Product Brief
A productive leather bag project begins with a brief that explains what the product needs to achieve, not simply what it should resemble. A reference photograph is useful for communicating style, but it rarely reveals the internal structure, thickness, seam construction, reinforcement, zipper specification, pocket depth, or hardware attachment. Two handbags that appear almost identical online may use completely different material combinations and production methods, which can create very different price, durability, weight, and production consistency.
The first brief should identify the product category, target user, sales channel, estimated quantity, size, color plan, use case, and expected quality level. A leather work tote intended to carry a laptop needs different reinforcement from a lightweight fashion tote. A small DTC crossbody bag may prioritize surface finish and packaging presentation, while a department-store program may place more emphasis on repeat-order consistency, barcode handling, carton specifications, and stable hardware availability. Manufacturing decisions become much easier once these commercial requirements are understood.
Dimensions should include more than overall width and height. For a handbag, useful measurements can include finished width, height, depth, handle drop, shoulder-strap range, zipper opening length, pocket dimensions, and major hardware positions. Capacity also matters because a bag that measures correctly may still perform poorly if the opening is too narrow, the interior pockets are inconvenient, or the base collapses when realistic contents are placed inside.
A practical first-stage brief usually includes:
- Bag category and intended use
- Finished width, height, and depth
- Handle drop or strap range
- Reference images, drawings, or physical sample
- Preferred leather direction
- Interior layout and lining
- Closure type
- Hardware finish
- Logo method and position
- Quantity by style and color
- Packaging requirement
- Destination market
- Required delivery window
Order quantity should be broken down by SKU whenever possible. A request for 1,000 units in one color is operationally different from 1,000 units divided among five colors, because smaller color runs can affect leather purchasing, hardware preparation, production changeovers, packaging, and the practical MOQ for custom components.
Turn References Into Specifications
Many companies assume that manufacturing cannot begin without a complete tech pack. A detailed tech pack is extremely useful, particularly for established brands, but product development can also start from a physical sample, sketch, reference photo, competitor product, concept drawing, or combination of those inputs. The important requirement is not that every specification exists at the beginning, but that the development process gradually removes uncertainty before production approval.
A visual reference must eventually become measurable. If a drawing shows a wide shoulder strap, the production specification still needs finished width, total length, adjustment range, leather thickness, reinforcement, buckle dimensions, edge treatment, stitching distance, and attachment method. If the reference shows a structured body, the team must determine whether that shape comes from firmer leather, bonded backing, foam, nonwoven reinforcement, board, or several layers working together.
Color and hardware require similar translation. “Dark brown leather with gold hardware” is an aesthetic description, not a production standard. Leather may differ by grain, finish, softness, coating, thickness, and dye lot. Gold hardware can vary from pale champagne to deep yellow gold, with different gloss levels, plating processes, weights, and base metals. A reliable development process converts these descriptions into approved physical or documented references before materials are ordered for bulk production.
A typical path from idea to production looks like this:
Reference or Concept → Dimensions → Material Direction → Construction Review → Pattern → Prototype → Revision → Final Sample → Production Standard
The purpose of this sequence is not to make development unnecessarily complicated. It is to prevent hidden decisions from being made informally on the production floor after the order has already become expensive to change.
Check Manufacturability Early
An attractive leather bag design can still be difficult, inconsistent, or unnecessarily expensive to manufacture. Experienced product development therefore includes a manufacturability review before the first serious production commitment. This review examines how leather thickness, fold radius, hardware placement, reinforcement, seam construction, and assembly order interact with the intended design instead of treating each component as an independent choice.
A thick leather may look premium as a material swatch but become bulky around a small zipper opening where several folded layers overlap. A narrow handle may appear elegant in a drawing but become uncomfortable or weak when the customer carries several kilograms. A large metal logo may look impressive from the outside but require backing on the inside to prevent the hardware from pulling through softer leather. These are easier problems to solve during development than after bulk materials have been purchased.
Manufacturability questions should include whether the leather can hold the desired silhouette, whether corners can be sewn cleanly, whether hardware can be installed without distorting the surrounding leather, whether handles have sufficient support, and whether the product can be reproduced at the target price. A design that requires excessive hand correction on every unit may produce a beautiful prototype but create serious consistency problems when the order scales.
Experienced development teams also check whether components are commercially realistic. A custom buckle or zipper puller may require tooling or a larger component MOQ than the bag quantity itself. A special leather color may require a minimum material purchase that makes a 200-piece trial order impractical unless excess material can be used later. Identifying these constraints early allows the design, material, or order plan to be adjusted before they become delays.
Which Leather and Components Should You Choose?

Leather should be selected according to the product’s structure, target price, desired appearance, durability, expected order volume, and tolerance for natural variation. Lining, reinforcement, hardware, thread, zippers, and branding should then be chosen as part of the same construction system. A premium hide cannot compensate for weak hardware, unsuitable reinforcement, or a component specification that cannot remain stable across repeat production.
Compare Leather by Real Performance
There is no single leather that is automatically best for every custom bag. Full-grain, top-grain, vegetable-tanned, pebbled, suede, PU, and microfiber leather can all be appropriate when matched to the right product. The useful comparison is not simply which material sounds most premium, but how each material behaves in cutting, folding, skiving, sewing, edge finishing, daily use, and future repeat orders.
Full-grain leather retains more natural surface character and is often selected for premium products where customers accept grain variation and natural markings as part of the material. That character also means selection and panel matching become more important. Large front panels may need to be cut from visually compatible areas, and usable yield can fall when the design allows only very clean surfaces.
Top-grain leather can offer a more refined and controlled appearance while retaining many of the tactile qualities associated with genuine leather. Pebbled leather is widely used for handbags because the textured grain can make small scratches and natural surface variation less obvious in daily use. Vegetable-tanned leather typically offers a firmer character and develops patina, which makes it suitable for heritage-inspired leather goods, straps, structured products, and certain premium accessories.
PU and microfiber materials are also practical tools rather than simply lower-priced substitutes. For some fashion and retail programs, the greater uniformity of color and texture can simplify bulk matching. Microfiber leather can provide a consistent surface and durable performance when the correct grade is selected, while PU can be suitable for price-sensitive programs where repeatability and styling flexibility are important.
| Material | Typical Character | Main Production Consideration | Common Application |
|---|---|---|---|
| Full-grain leather | Natural, premium, develops character | Greater shade and grain variation | Premium totes, briefcases, travel goods |
| Top-grain leather | Refined, controlled surface | Grade and finish need clear approval | Handbags, business bags |
| Pebbled leather | Textured, practical | Grain scale should remain compatible | Everyday handbags |
| Vegetable-tanned leather | Firmer, develops patina | Fold and edge behavior need testing | Structured goods, straps |
| Suede | Soft, tactile | Surface marks during handling | Fashion products, trims |
| PU leather | Uniform, cost-efficient | Surface and backing vary by grade | Fashion and promotional ranges |
| Microfiber leather | Uniform, durable alternative | Supplier article should be controlled | Branded volume programs |
Szoneier’s documented leather capabilities include genuine leather, PU, and microfiber options, with leather projects requiring attention to material grade, texture, color variation, thickness, edge finishing, hardware, logo treatment, and batch consistency. The decision should therefore be made around the finished product and commercial requirement rather than around a material name alone.
Control Thickness, Grain, and Color
Leather thickness affects almost every later manufacturing operation. Softer fashion bags commonly use relatively flexible leather, often combined with hidden reinforcement, while structured business bags may use firmer material or additional supporting layers. As a broad development reference rather than a universal rule, many handbag constructions may use leather around approximately 0.8–1.2 mm, while straps, firmer panels, or structured leather goods can require heavier material or carefully laminated construction.
The important measurement is not only the thickness of a single leather layer. Once an edge is folded, a reinforcement layer added, lining included, and seam allowances stacked together, the final joint may contain several times the original material thickness. A leather that feels ideal on a flat table can therefore become too bulky in a small corner or around a zipper opening. Skiving is used to reduce thickness in controlled zones so folds and seams remain clean without weakening the product.
Grain should also be treated as a design standard. Natural leather is not perfectly uniform, but a large front panel with very fine grain beside a side gusset with unusually coarse grain can make a finished bag look inconsistent. Premium projects may therefore define different acceptance levels for highly visible panels and hidden components so natural material can be used efficiently without sacrificing appearance.
Color control should rely on physical approval rather than color names alone. “Tan,” “camel,” “cognac,” and “dark brown” can cover many visually different shades. Surface finish changes color perception as well; matte, semi-gloss, waxed, and heavily pebbled leather can make similar dye formulas look different under the same light. Repeat-order programs benefit from keeping the supplier article, approved swatch, thickness range, surface finish, and acceptable variation in the project record.
Match Hardware and Reinforcement to the Bag
Customers often notice hardware first because buckles, D-rings, zipper pullers, clasps, magnetic snaps, and metal logos contribute heavily to the visual identity of a leather bag. From a manufacturing point of view, however, hardware should be evaluated not only by appearance but also by size, base metal, plating, weight, function, attachment method, and the forces it transfers into the surrounding leather.
Handle and strap attachments are especially important. A work tote carrying a laptop, charger, water bottle, and other daily items may regularly carry several kilograms. The leather body itself may be strong enough while the handle anchor becomes the weakest point. Reinforcement can be placed behind handle bases, D-ring tabs, rivets, magnetic snaps, zipper ends, and bag bottoms so the loads are spread across a larger area rather than concentrated on one small piece of leather.
The correct reinforcement should support the function without destroying the desired feel. Over-reinforcing every panel can make a handbag heavy and stiff, while under-reinforcing stress points creates premature wear. A soft hobo bag and a structured business tote should not use the same reinforcement strategy simply because they are similar in size.
Logo treatment also needs testing on the actual material. Embossing depth changes according to leather firmness and grain. Foil stamping depends on the surface coating, pressure, temperature, and foil compatibility. Metal logos need secure backing while keeping the outside panel smooth. These details should be confirmed on the sample rather than assumed from a logo artwork file.
How Are Custom Leather Bag Samples Developed?

Sampling turns the design into a physical product that can be measured, carried, opened, loaded, inspected, revised, and approved. A complete sampling process normally includes pattern development, material preparation, first prototype construction, functional review, documented corrections, and final approval. The sample should prove not only appearance, but also dimensions, usability, materials, hardware, structure, workmanship, cost practicality, and repeatability.
Build the Pattern Around Construction
Pattern making is the point where a three-dimensional bag begins to become a manufacturing system. Each visible and hidden component may require an individual pattern, including front and back panels, gussets, bottom, zipper panels, pockets, lining sections, handles, straps, flaps, piping pieces, reinforcement, and decorative components. The pattern has to define how those pieces meet, not merely trace their final visible shape.
Finished measurements are different from cutting measurements. A leather tote described as 35 × 30 × 12 cm still requires seam allowances, fold allowances, zipper construction, gusset geometry, edge-finishing allowances, and turning radii. If the side gusset is only a few millimeters wrong, the final depth can shift, the top zipper may become difficult to install, or the bag can appear twisted after assembly.
Leather adds another consideration because needle holes and cutting errors are difficult to hide. Woven fabric can sometimes tolerate small corrections during sewing, while forcing a leather panel into a mismatched seam can distort grain or create permanent tension. Accurate pattern development therefore reduces both material waste and workmanship problems.
The first sample often exposes issues that drawings cannot predict. A pocket may technically fit the measurements but feel awkward in actual use. A zipper may look correct but not open wide enough for the intended contents. A corner may require excessive manipulation during sewing. The sample should be treated as an engineering test that feeds information back into the pattern rather than simply as a visual mock-up.
Review the Sample Under Real Use
The first physical sample should be reviewed with measurements, hands, and realistic contents rather than only through photographs. Begin by checking width, height, depth, handle drop, strap range, pocket positions, zipper opening, and major hardware locations. Then use the bag in the same way a customer will use it because functional problems are often difficult to identify while the product is sitting empty on a table.
A work tote should be tested with representative contents such as a laptop, notebook, charger, bottle, and personal items. A crossbody bag should be worn at different strap settings to see whether the buckle location is comfortable and whether the bag tilts. A travel bag should be opened and packed to determine whether access, zipper movement, handle position, and internal organization work in practice.
The sample should then be evaluated in four areas: appearance, function, construction, and manufacturability. Appearance covers silhouette, symmetry, grain, color, edge finish, logo, and hardware. Function covers closures, capacity, pockets, carrying comfort, and access. Construction covers reinforcement, seams, lining, and hardware anchoring. Manufacturability asks whether the same result can be repeated efficiently across the planned order quantity.
Revision comments should be measurable whenever possible. “Make the handle stronger” leaves too much interpretation. “Increase finished handle width from 18 mm to 22 mm and add reinforcement behind both anchor zones” gives the pattern and sampling teams a specific action. Clear revisions reduce unnecessary sampling cycles and improve the chance that the next prototype addresses the real issue.
Approve a Production Standard
The last development sample should become a controlled reference for production rather than an attractive object that disappears after marketing photography. A strong approval package combines the physical sample with the final pattern revision, measurement sheet, leather reference, hardware standard, artwork, logo placement, edge-finish details, packaging specification, and a record of changes made during sampling.
A typical custom leather bag development sequence can be managed as follows:
| Stage | Purpose | Practical Output |
|---|---|---|
| Product review | Confirm feasibility and commercial direction | Material and structure plan |
| Pattern development | Translate dimensions into components | Pattern set |
| First prototype | Test structure and workmanship | Physical sample |
| Revision | Correct functional and visual issues | Updated specification |
| Final sample | Confirm finished product | Approval reference |
| Pre-production confirmation | Lock standards before bulk | Production-ready specification |
Szoneier’s documented sampling process moves from material confirmation through pattern making, sample sewing, internal checking, review, revision, and final approval, creating a controlled reference before bulk production. For selected leather bag projects, documented sample development can be around 10–15 days, although custom hardware, special leather colors, complex structures, and additional revision rounds can extend the schedule.
Bulk production should not begin while important sample decisions remain unresolved. A small problem repeated once on a prototype is manageable; the same problem repeated across hundreds of finished bags becomes a commercial issue involving rework, delivery delays, freight, and sometimes lost selling time. The final sample is therefore one of the most important risk-control tools in custom manufacturing.
How Are Custom Leather Bags Manufactured?
Bulk leather bag manufacturing normally moves through incoming material inspection, pattern preparation, cutting, skiving, reinforcement, logo application, component preparation, sewing, lining assembly, hardware installation, edge finishing, shaping, cleaning, final inspection, and packaging. The exact order depends on the design, but each operation should follow the approved sample and controlled specification rather than the memory or personal interpretation of individual workers.
Inspect, Cut, and Skive the Leather
Genuine leather requires inspection before cutting because hides naturally vary in shape, grain, thickness, elasticity, scars, wrinkles, and surface character. The cutting team identifies which areas are appropriate for highly visible panels and which areas can be used for smaller or hidden components. The objective is not to eliminate all natural variation, but to keep the finished product within the appearance standard approved during sampling.
Panel placement is particularly important on premium bags with large uninterrupted surfaces. A front body panel and matching back panel may need compatible grain and shade, while a small internal tab can accept a broader range of natural appearance. If every square centimeter is held to the same cosmetic standard, usable leather yield can fall sharply and product cost can increase without a meaningful improvement for the customer.
Leather cutting can be completed using dies, presses, hand tools, or digital cutting systems depending on the material, order quantity, and design. Precision remains essential regardless of equipment because dimensional errors accumulate during assembly. A gusset that is only slightly too long can create waviness around the body seam, while an incorrectly cut zipper panel can affect both the bag opening and final symmetry.
Skiving follows on selected areas to reduce thickness where leather folds, overlaps, wraps reinforcement, meets zipper tape, or enters a seam with several layers. Too little skiving creates bulky joints and difficult sewing. Too much removes strength and can create weak edges. Experienced preparation therefore controls both the width and depth of skiving according to the leather, construction, and finished appearance required.
Reinforce, Sew, and Assemble the Bag
Leather bags often contain far more hidden material than customers realize. Reinforcement, foam, backing, tapes, boards, zipper tapes, lining, adhesives, pocket panels, and hardware supports may all be prepared before the outside body is finally assembled. This hidden structure determines how the bag behaves in use, whether it stands or collapses, and whether handles and closures survive repeated loading.
The assembly sequence is usually designed around access. An internal pocket is easier to sew while the lining panel is still flat. A logo may need to be embossed before reinforcement is bonded behind the leather. Zipper panels can be completed as subassemblies before being joined to the main body. Handles and straps are often produced separately so their reinforcement, folds, stitching, edge finish, and hardware can be controlled before final attachment.
Handle engineering deserves particular attention because the finished component can contain several layers. A leather handle may include outer leather, inner reinforcement, filler, folded edges, adhesive, and stitching. Shoulder straps can add adjustment hardware, holes, keepers, and swivel hooks. Their load-bearing points should be designed as structural parts of the product rather than decorative additions.
Visible stitching needs careful machine setup because leather remembers every needle hole. Removing an incorrect stitch line can leave permanent perforations even after the thread is gone. Stitch length, tension, needle size, thread, presser-foot setup, edge distance, and corner handling should therefore be confirmed before significant quantities are sewn. In-process inspection is especially valuable during early production because correcting a machine setting after 20 pieces is much easier than correcting it after 1,000.
Finish Edges and Final Details
Edge finishing is one of the areas experienced customers often inspect first because it reveals how much control exists behind the finished product. Leather edges may be turned, folded, bound, left intentionally raw, or finished with edge paint. Painted edges can require preparation, sanding, base coating, drying, additional paint applications, and polishing depending on the product standard and leather type.
Good edge paint should look smooth and consistent without becoming excessively thick or plastic-like. Common problems include rough sanding, pinholes, uneven thickness, overflow, cracking, peeling, color mismatch, and poorly finished corners. Handles and shoulder straps deserve especially close attention because these areas are frequently touched and flexed during use, which makes weak finishing more noticeable over time.
Final assembly also includes checking hardware installation, zipper movement, strap adjustment, loose threads, adhesive marks, scratches, protective films, shape, stuffing, and cleanliness. The product should be examined from normal customer distance as well as close range. A seam can technically pass measurement checks while still making the bag look visually unbalanced if one side sits higher or the logo is slightly off-center.
Leather products tend to receive closer tactile inspection than many basic fabric bags because customers expect surface quality, edge quality, hardware, and stitching to justify the material and price level. Finishing therefore cannot be treated as a cosmetic afterthought. It is part of the construction system and should be approved, documented, and inspected just like measurements or materials.
How Is Leather Bag Quality Controlled?

Leather bag quality control should begin before production and continue through material inspection, cutting, sewing, assembly, finishing, final inspection, and packaging. Each stage should be compared against approved materials, measurements, construction, hardware, logo, edge finishing, functionality, and packing standards. The purpose is to prevent a defect from multiplying throughout the order rather than relying on one inspection after every bag has already been finished.
Control Materials Before Cutting
The first major quality checkpoint happens before leather reaches the cutting table. Material should be compared with the approved reference for color, grain, thickness, surface finish, softness, and acceptable natural characteristics. Hardware should be checked for dimensions, finish, plating tone, scratches, function, and attachment compatibility. Linings, zippers, reinforcement, thread, labels, and packaging should also match the specifications used for the approved sample.
This stage prevents one of the most expensive manufacturing problems: excellent workmanship applied to the wrong material. If a different leather batch feels noticeably softer or darker than the approved sample, no amount of careful sewing can make the finished bags identical. The discrepancy needs to be identified before material is converted into components and before the cost of correction increases.
Batch control becomes especially important when a large order uses leather from several production lots. Genuine leather naturally allows some variation, but finished bags placed beside each other in retail stores or product photography should still look like the same SKU. Materials can therefore be grouped, compared, and allocated carefully before cutting to prevent obvious shade or grain jumps within individual products.
Szoneier’s documented custom bag QC system includes raw-material inspection, accessory checking, pre-production sample confirmation, cutting inspection, sewing-process inspection, semi-finished inspection, final inspection, and packaging inspection. The value of this sequence is that every stage catches a different category of problem before more labor and material are added.
Inspect the Critical Leather Details
Leather-bag inspection must combine cosmetic standards with functional standards. Visible leather is checked for unacceptable scratches, scars, stains, shade variation, grain mismatch, surface damage, and handling marks. Natural variation should be judged against the approved leather rather than against an unrealistic expectation of perfect uniformity, because excessive rejection of normal material character can raise cost without improving actual product performance.
Stitching should be examined for even stitch length, tension, seam position, skipped stitches, loose threads, waviness, back-tacking, and clean corner transitions. On premium leather products, visible stitch lines often contribute to the design itself, which means small irregularities become easier to notice than they would on a heavily textured technical fabric.
Edge paint requires separate inspection because it can fail in several ways. Inspectors look for adhesion, smoothness, color, thickness, cracking, peeling, overflow, pinholes, rough sanding, and unfinished corners. Handles and straps may be flexed or handled during inspection because an edge that looks acceptable while flat can reveal weakness once the component bends.
Hardware is checked for appearance, location, operation, and security. Zippers should move smoothly, magnetic snaps should align, swivel hooks should rotate correctly, buckles should adjust, and rivets or screws should remain secure. The quality of the metal itself is only half of the problem; the way the fitting is attached to leather is equally important.
| Inspection Area | What Is Checked | Typical Risk |
|---|---|---|
| Leather | Shade, grain, surface, thickness | Mismatched panels or surface defects |
| Dimensions | Width, height, depth, straps | Finished product outside tolerance |
| Stitching | Alignment, tension, stitch length | Wavy or skipped stitching |
| Edge finish | Adhesion, smoothness, color | Cracking or peeling |
| Hardware | Finish, position, operation | Scratches, looseness, poor alignment |
| Handles and straps | Attachment and reinforcement | Load-bearing failure |
| Lining | Fit, seams, pocket position | Wrinkles or loose construction |
| Logo | Position, depth, finish | Inconsistent brand presentation |
| Structure | Shape, symmetry, loaded behavior | Sagging or twisting |
| Packaging | Protection, label, carton setup | Damage or shipping error |
The most critical checkpoints should change according to the product. A leather backpack demands careful shoulder-strap and load-bearing inspection, while a structured handbag may require tighter cosmetic control around symmetry, edge paint, metal placement, and the way the body stands when empty.
Keep Bulk Production Close to the Sample
Sample-to-bulk consistency is not created by asking the production team to “make it like the sample.” The approved physical sample should be supported by information that different departments can use: final patterns, measurements, leather references, hardware specifications, logo artwork, edge-finish standards, reinforcement details, packaging instructions, and a record of approved revisions.
Bulk production introduces more variables than sampling. Several operators may work on the order, leather can come from multiple hides or lots, production can run over different days, and different inspectors may evaluate the product. Each undocumented detail increases the chance that interpretation changes as the order moves through the factory.
Production references should therefore be available during cutting, sewing, assembly, and inspection rather than kept in an office until final QC. Early finished pieces can be checked against the approved sample so that issues with shape, stitch position, reinforcement, hardware, or edge finishing are corrected while only a small percentage of the order has been completed.
Repeat orders create another form of risk. Months later, the exact leather lot may no longer be available, plating can vary slightly between hardware batches, and component suppliers can modify products. Stable repeat production depends on retaining the previous specification and reviewing any necessary substitutions before manufacturing begins. For brands building permanent products or seasonal collections, this record becomes a long-term supply-chain asset rather than just paperwork.
What Should You Confirm Before Ordering?
Before placing a bulk order, confirm the approved sample, final specification, quantity by SKU, price basis, material standard, hardware, packaging, production lead time, inspection method, shipping plan, and rules for any changes. A good order should describe one clearly defined product so the factory, brand, quality team, and logistics team are all working from the same expectations before materials and production capacity are committed.
Understand MOQ, Cost, and Lead Time
MOQ for a leather bag is influenced by much more than how many pieces a sewing line can produce. Leather availability, custom color requirements, zipper purchasing, hardware quantities, logo tooling, packaging, and the number of colors or styles can all determine the practical minimum for a particular project.
A factory may be comfortable sewing 200 bags while the supplier of a custom metal zipper pull requires a larger quantity. A specially dyed genuine leather may also have a minimum material purchase that exceeds the leather actually needed for a small first order. In these situations, a manufacturer can sometimes suggest existing hardware, standard leather colors, PU, microfiber, or other alternatives that make a lower-volume trial commercially more practical.
Unit price should also be understood as the combination of material and construction rather than as the price of leather alone. Leather usage, usable cutting yield, lining, reinforcement, zippers, hardware, sewing labor, skiving, edge finishing, logo processes, packaging, and order quantity all influence cost. Large uninterrupted panels can increase leather consumption because natural defects and irregular hide shapes reduce usable yield.
Selected Szoneier leather-bag projects currently document MOQ from around 200 pieces, with sampling around 10–15 days and bulk production around 35–60 days, depending on the leather, hardware, structure, lining, logo, packaging, SKU configuration, and material readiness. These figures are working project ranges rather than universal guarantees, because custom metal molds, special leather development, repeated sample revisions, laboratory testing, or complex packaging can add additional time.
Lead time is clearer when broken into stages:
Design Review → Material Confirmation → Sampling → Revision → Approval → Material Preparation → Bulk Production → Inspection → Packing → Shipment
This approach makes delays easier to identify and manage. A 50-day manufacturing program does not mean every day is spent sewing; a significant part of the schedule can be consumed by leather preparation, hardware production, approval, and packaging materials.
Evaluate the Manufacturer Beyond Price
A low quotation can be attractive during supplier comparison, but it does not automatically create the lowest total sourcing cost. If leather must be replaced after sampling, hardware plating fails in production, dimensions drift, or finished bags need rework before shipment, the commercial impact can quickly exceed the difference between two original quotations.
A useful factory evaluation therefore focuses on whether the team can explain how the product will be developed and controlled. Ask who develops the pattern, how leather batches are reviewed, how sample revisions are recorded, where reinforcement is placed, how hardware is approved, when production inspection happens, and what information is retained for repeat orders.
Technical questions often reveal more than a polished company presentation. A knowledgeable team may explain that a selected leather is too thick for the proposed folding construction, that a particular custom buckle will make the MOQ impractical, or that a shoulder-strap anchor needs a wider reinforcement patch. Those comments may create additional decisions during sampling, but they often prevent larger problems later.
The ability to identify risk is therefore a positive signal. Manufacturing is not a process in which every idea should receive an immediate “yes.” Strong factories are willing to explain which design choices are expensive, unstable, difficult to repeat, or poorly matched to the planned quantity, and then offer practical alternatives that protect the intended design as much as possible.
Send Enough Information for an Accurate Quote
A quotation based only on a photograph can be useful as an early estimate, but it should not be treated as the final production price. Without measurements, leather specification, quantity, lining, hardware, logo, pockets, reinforcement, packaging, and destination information, the factory has to make assumptions that may later change the cost substantially.
For a serious custom leather bag quotation, provide a tech pack, drawing, product photo, reference sample, or clear concept together with finished dimensions and estimated order quantity. Indicate the leather direction, number of colors, lining requirement, hardware finish, strap or handle construction, logo method, packaging expectations, destination market, and required delivery timing. If some details remain open, state that they are open so the manufacturer can present alternatives instead of silently choosing a specification.
A useful request might say that top-grain leather is preferred but microfiber should also be quoted as a more consistent or cost-controlled alternative. This allows the supplier to build a meaningful comparison. A request that simply asks for “the best leather quality at the lowest price” creates conflicting priorities and gives very little technical basis for quotation.
Target pricing can also be helpful when it reflects a real commercial requirement. A premium genuine-leather handbag may justify higher leather and hardware costs, while a fashion program with broader distribution may need tighter cost control and higher batch consistency. A manufacturer can make better material and construction suggestions when the target market is understood.
Before a bulk-order deposit is paid, the approved sample, quotation, specification, quantity, material, logo, packaging, and delivery terms should all describe the same product. When these records match, production becomes much more predictable. When they do not, disagreements usually appear only after materials have been purchased or finished bags have already been made.
Final Thoughts
Manufacturing a custom leather bag is not one production operation. It is a chain of decisions that begins with the product concept and continues through material selection, pattern engineering, sample approval, leather cutting, reinforcement, sewing, hardware installation, edge finishing, inspection, packaging, and repeat-order control. The strength of the finished product depends on how well those decisions work together rather than on any single impressive material or manufacturing process.
The most successful projects usually spend more effort removing uncertainty before bulk production. Leather grade is approved, grain and color expectations are understood, hardware is confirmed, patterns are corrected through sampling, stress points are reinforced, workmanship is defined, and production teams have a real reference to follow. This preparation may appear slower than moving immediately from a drawing to a purchase order, but it usually saves time when the cost of mistakes becomes much higher.
For brands developing leather totes, handbags, backpacks, pouches, business bags, or related leather goods, Szoneier can work from product ideas, reference samples, drawings, and technical packages and connect material sourcing, sample development, manufacturing, quality control, packaging, and delivery within the same project workflow. The real value of this approach is not simply producing the first order; it is creating a product standard that can be repeated, improved, and scaled as the product line grows.
Frequently Asked Questions
How long does it take to manufacture a custom leather bag?
Custom leather bag timing depends on the material, construction, hardware, sample revisions, packaging, and order size. A relatively straightforward project may require around 10–15 days for sample development and roughly 35–60 days for bulk production after approval, while special leather colors, custom hardware, testing, complex edge finishing, or several revision rounds can increase the total project time. Material preparation should always be separated from actual sewing time when planning a launch.
What is the typical MOQ for custom leather bags?
MOQ varies according to leather availability, color quantity, custom hardware, logo process, packaging, and construction. Some custom leather projects can begin around 200 pieces, but the practical minimum can increase when a special leather color, metal mold, zipper puller, gift box, or other component has its own purchasing requirement. Using available leather colors, standard hardware, PU, or microfiber can sometimes make smaller trial orders easier to execute economically.
Which leather is best for custom handbags?
There is no single best material for every handbag. Full-grain leather works well when natural character and premium positioning are important, while top-grain leather can provide a more refined surface. Pebbled leather suits practical everyday bags, vegetable-tanned leather fits firmer products, and microfiber or PU can offer better consistency for some volume programs. The choice should consider appearance, thickness, structure, price, cutting yield, intended use, and repeat-order requirements together.
How much does it cost to manufacture a custom leather bag?
The manufacturing cost depends on leather type and usage, cutting yield, lining, reinforcement, zipper and hardware specifications, construction complexity, sewing labor, edge finishing, logo process, packaging, and quantity. A large genuine-leather tote with custom metal hardware and painted edges will normally cost significantly more to manufacture than a small PU pouch with standard components. Accurate costing therefore requires dimensions, materials, construction, branding, packaging, and quantity rather than only a reference photo.
Do I need a tech pack to manufacture leather bags?
A complete tech pack is highly useful but not always required to begin development. A manufacturer can often start from a physical sample, sketch, photo, reference product, or concept and then help convert those inputs into dimensions, materials, patterns, hardware, construction, and sample specifications. What matters is that the information becomes controlled before bulk production. The final approved sample and supporting specification should remove most important interpretation before materials and production capacity are committed.
How do manufacturers keep bulk leather bags consistent with the sample?
Consistency comes from controlling the variables that created the approved sample. The factory should retain the final pattern, measurements, leather reference, hardware standard, logo artwork, reinforcement details, edge-finish requirement, packaging instructions, and revision history. Bulk materials should be checked before cutting, early production pieces compared with the approved sample, and inspections performed during sewing, assembly, final finishing, and packaging rather than relying only on one final check.
Should I choose genuine leather, PU, or microfiber leather?
Choose according to product positioning rather than assuming one material is always superior. Genuine leather offers natural texture, premium perception, and distinctive aging characteristics, but it normally requires greater control of grain, shade, thickness, and yield. PU can provide competitive cost and surface consistency, while higher-grade microfiber can deliver durability and stable appearance for repeat production. Testing actual material swatches and prototypes is usually more useful than choosing only from material names or online photographs.