Skip to content

A product collection can look beautifully coordinated on a computer screen and still feel strangely disconnected once the physical samples arrive. The backpack may use matte black zipper pullers while the travel pouch comes with glossy black hardware. A carefully selected navy may look rich on nylon, warmer on canvas, and almost purple on a molded rubber patch. The logo that looked balanced on a 45 cm duffle may suddenly dominate a 16 cm organizer. None of these differences seems serious in isolation, yet together they can make a product line look less considered and less valuable.
Brand consistency across bag accessories comes from defining a repeatable product language for colors, materials, logos, hardware, trims, labels, packaging, workmanship, and production references. The goal is not to make every SKU identical. Brands need to decide which elements remain fixed, which can adapt to product function and size, and how every approved decision will be documented, sampled, inspected, and reproduced in later orders.
Picture a travel collection containing a backpack, weekender, toiletry bag, packing cube, passport wallet, cable organizer, luggage tag, and detachable strap. A customer should be able to place those eight products on one table and recognize that they belong to the same family before reading a single hangtag. Achieving that result is not simply a graphic-design exercise. It requires material judgment, component planning, logo engineering, physical sampling, specification control, manufacturing discipline, and a clear record of what was finally approved.
What Makes Bag Accessories Feel Consistent?
Bag accessories feel consistent when different products repeat the same recognizable design language through color, material character, logo treatment, hardware finish, trim details, packaging, and workmanship. Consistency does not require identical products. It means a backpack, pouch, wallet, travel organizer, strap, and small leather accessory can serve different functions while still looking and feeling as though they were developed for the same brand.
Shared Design Language
Strong product families usually rely on several repeated cues rather than one oversized logo. Customers notice the shell material, zipper puller, webbing, lining, stitch appearance, hardware surface, edge treatment, branding method, and package presentation almost immediately. When these details speak the same visual language, even products with very different structures can feel closely related. When they conflict, adding more logos rarely fixes the problem.
A useful starting point is to define five to eight elements that customers should repeatedly encounter across the collection. These might include one primary color family, a defined hardware finish, an approved group of logo applications, a recognizable webbing style, a lining direction, a limited trim palette, common packaging graphics, and a consistent workmanship level. Those elements become the collection’s visual grammar, while individual products remain free to solve different functional needs.
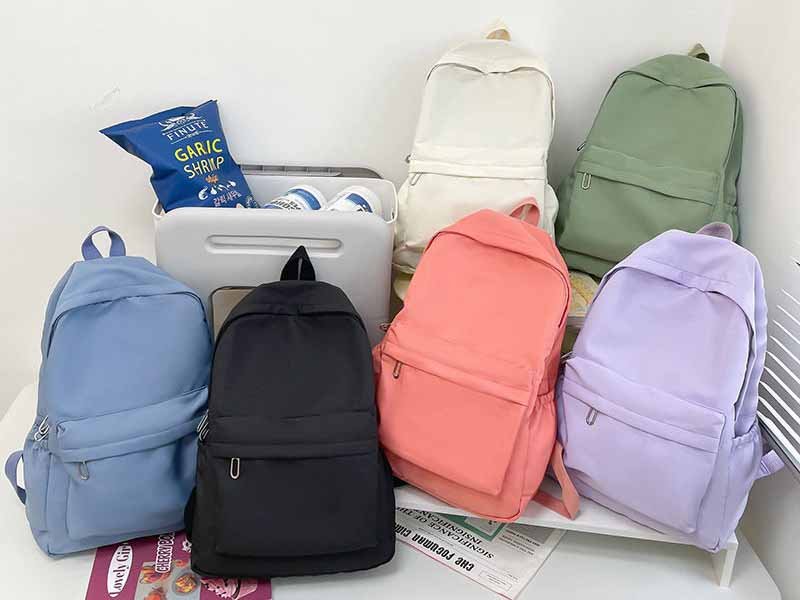
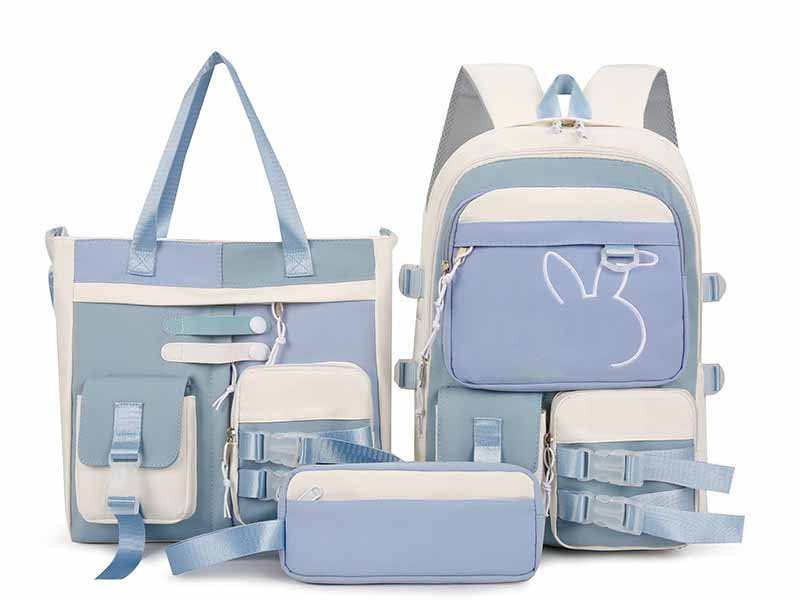
Consider a travel range built from four materials: nylon for the backpack, polyester for packing cubes, PU for the luggage tag, and canvas for an accessory pouch. The materials do not match, but the range can still feel unified if all four products share a restrained navy-and-black palette, matte hardware, related zipper pullers, similarly scaled logos, clean tonal stitching, and the same packaging hierarchy. The material changes because the functions change; the product language remains recognizable.
This distinction becomes more important as a collection expands. Szoneier’s company documentation describes its role in helping brands develop product lines around consistent material, logo, structure, and packaging direction rather than treating each SKU as an unrelated order. That manufacturing approach reflects a practical reality: consistency is easier to protect when common rules are agreed before individual products begin to multiply.
Fixed and Flexible Elements
Product teams often run into trouble because they have not decided which specifications are brand rules and which are product rules. A logo proportion, primary color direction, hardware family, and packaging system may need to stay closely controlled. Fabric weight, zipper size, reinforcement, strap width, foam thickness, and internal organization should usually respond to the intended function of each SKU.
A useful development system separates fixed elements from adaptive elements. Fixed elements create recognition. Adaptive elements allow the product to work properly. The two categories should be documented differently, because treating everything as fixed can make new products awkward, while treating everything as flexible eventually causes brand drift.
| Element | Typical Control | Practical Application |
|---|---|---|
| Master logo artwork | Fixed | Approved proportions used across every SKU |
| Primary brand color | Fixed direction | Physically matched on each material type |
| Hardware finish | Mostly fixed | Matte black, gunmetal, brushed nickel, or another approved family |
| Logo dimensions | Adaptive | Smaller on pouches, larger on backpacks and duffles |
| Fabric weight | Adaptive | Selected according to structure, load, and intended use |
| Webbing width | Adaptive | Approximately 15–20 mm for small details, 25–50 mm for larger straps |
| Packaging graphics | Fixed | Same logo hierarchy, type system, and visual language |
| Product construction | Adaptive | Different gussets, pockets, straps, reinforcements, and closures |
The figures above are practical industry ranges rather than universal rules. A lightweight pouch may need a completely different webbing width and material construction from a travel duffle. What matters is that the reason for the difference is clear. Customers should perceive the change as functional adaptation rather than as a random shift in quality, color, finish, or design direction.
A Collection Is Not a Set of Clones
Brand consistency is often misunderstood as repetition. That can lead to a 70 mm logo being placed on both a large weekender and a compact makeup pouch, or a heavy metal zipper pull being used on a lightweight organizer simply because the large bag uses it. The result may technically be consistent, yet visually and functionally it can feel less sophisticated.
Experienced bag development works with proportional consistency. A logo may range from 25 mm on a small accessory to 80 mm or more on a large travel bag, but its relative prominence remains comparable. A strap may use 20 mm webbing on a small pouch and 38 mm webbing on a duffle, yet the weave, color family, and surface quality can still be closely related.
The same thinking applies to materials. One SKU may need a lightweight 210D or 420D woven material, another may use 600D Oxford, while a premium small accessory might use PU or genuine leather. Forcing one substrate onto all three products would make little sense. What the brand should preserve is a recognizable relationship in sheen, color, surface character, trims, branding, and finishing.
Physical range reviews are particularly valuable at this stage. Samples that appear acceptable when viewed separately can reveal obvious differences when arranged together. A zipper suddenly looks too shiny, one logo appears oversized, one fabric is noticeably warmer in color, or a lining looks cheaper than everything around it. Customers eventually see products together on category pages, shelves, campaign images, bundles, and merchandising tables, so product teams should evaluate them the same way.
Which Brand Elements Should You Standardize?
The elements worth standardizing are the details customers repeatedly see and touch: core colors, logo artwork, hardware finishes, zipper treatments, webbing, lining direction, labels, stitching character, packaging, and workmanship expectations. These should have clear master references, while individual SKU specifications explain where changes are allowed to accommodate product dimensions, function, material behavior, target cost, and production requirements.
Colors and Surface Finishes
Color is one of the strongest brand identifiers and one of the easiest details to underestimate during manufacturing. A brand may nominate one Pantone reference, but that reference will not automatically produce an identical visual result on nylon, polyester, cotton canvas, PU leather, rubber, silicone, zipper tape, woven webbing, painted metal, and printed paper packaging. Each substrate interacts with light and color differently.
For this reason, digital references should be treated as the beginning of color communication rather than the final approval. A more dependable sequence uses a master reference, physical material swatches, trim samples, finished prototypes, and a bulk-production comparison standard. When a signature color matters, it is worth placing the actual fabric, zipper tape, webbing, label, logo component, and hardware next to each other before the production order is released.
Szoneier’s documented color-control process includes Pantone referencing, material swatch approval, sample confirmation, bulk fabric batch checks, zipper and webbing matching, logo color checking, and final comparison with approved samples. That sequence is useful because it moves color control from an abstract number to the actual combinations a customer will see on a finished bag.
The goal is not always perfect spectral matching. Tonal products often use intentionally different shades, and some materials cannot reproduce another substrate exactly. The more useful question is whether the complete color relationship looks deliberate. A slightly darker zipper tape against a navy shell can look refined, while an unintended purple cast in one component may make the product appear poorly controlled.
Hardware should be standardized with similar care. “Black hardware” is not a detailed specification. Glossy black, matte black, gunmetal, electrophoretic black, powder-coated black, and black plastic can look noticeably different. The same applies to silver, nickel, gold, brass, and antique finishes. A collection can use different hardware sizes and constructions, but the visible surface direction should usually remain within an intentional family.
Zippers, Webbing, and Linings
Zippers are sometimes treated as basic functional components, yet they have a surprisingly large influence on how a bag looks and feels. A zipper specification can involve chain type, coil size, tape color, slider finish, puller shape, opening direction, and customized branding. Two products using black zippers can still appear unrelated when one has glossy plated pullers and the other uses matte molded pullers.
Webbing deserves similar attention because it may cover a significant percentage of the visible product. Backpack shoulder straps, compression straps, carry handles, zipper extensions, attachment loops, and removable straps can all introduce different textures and shades. Switching from a dense nylon weave to lightweight polypropylene can noticeably change perceived quality even if both pieces are technically the same color.
Practical webbing widths in bag development often range from about 15 mm for small loops and accessory details to 25 mm for compact shoulder straps and 38–50 mm or more for larger handles or load-bearing straps. Those numbers are not quality grades; the correct specification depends on product size, expected load, construction, appearance, and the type of hardware the webbing must pass through.
Linings provide another opportunity to build recognition. Some brands maintain a single neutral lining direction, while others use a distinctive contrast color or subtle repeat print that becomes recognizable each time the bag is opened. The material itself can still change. A cosmetic pouch may need a wipe-clean lining, while a travel backpack can use lightweight woven polyester. Consistency lies in the visual language rather than blindly repeating one fabric construction.
Labels and Packaging
Packaging becomes increasingly important when a product line is sold through retail, e-commerce, gifting, subscription, or DTC channels. A backpack and a small wallet rarely need the same package dimensions, yet the logo hierarchy, typography, information structure, material character, barcode logic, and brand color system should still feel related when the products arrive together.
A practical packaging system can standardize logo placement rules, typography, hangtag proportions, care-information style, barcode zones, product naming, material disclosure, and channel-specific labels. The package size then changes according to the product. This approach keeps visual recognition stable without creating inefficient packaging simply to make every box or polybag look identical.
SKU complexity can increase faster than expected. Ten product styles offered in four colors already create 40 style-color combinations before size, regional labeling, Amazon identifiers, retail barcodes, or packaging variations are considered. Informal file names and verbal descriptions become increasingly risky at that point, especially when several products are developed simultaneously.
Labels should also be treated as real product components. A woven label has a different edge, thickness, fold, and visual density from a heat-transfer label. A PU patch has different limitations from embroidery. Their dimensions, fold types, seam positions, backing, colors, and artwork should be confirmed during sampling rather than added as a final graphic detail just before bulk production.
How Do Materials Affect Brand Consistency?
Materials influence much more than durability. They change color appearance, sheen, texture, stiffness, silhouette, hand feel, logo performance, weight, and perceived price. A consistent collection can use many different substrates, but those substrates should follow a common visual and tactile direction. Important colors and branding should be physically approved on each material because a screen reference cannot show how a finished substrate will actually behave.
Color Changes Across Substrates
The same target navy can look completely different on 600D polyester, smooth nylon, washed canvas, PU leather, silicone, and woven webbing. A tightly woven synthetic fabric can reflect more light than cotton. PU coatings may increase saturation and gloss. Neoprene tends to soften the visual effect of a color, while molded rubber relies on pigmentation and surface texture rather than conventional textile dyeing.
Problems become more noticeable when several supposedly matching materials touch each other. A backpack might contain a navy shell, navy zipper tape, navy webbing, navy embroidery thread, and a navy rubber patch. If all five are sourced only by a verbal color name, the finished product can easily contain several different shades that were never evaluated together.
A more useful approval path is master reference → material swatch → trim sample → finished prototype → bulk-lot comparison. Each stage answers a different question. The reference establishes the intended direction, the swatch tests the substrate, the trim samples reveal component relationships, the prototype shows the complete product, and the production comparison checks whether the approved appearance is being repeated.
Brands should also decide where variation is acceptable. An exact tonal match may be important for zipper tape sitting directly beside the shell, while a slightly darker interior lining may be intentional. The standard should communicate the desired visual relationship rather than simply instructing every supplier to make “the same navy.”
Weight, Texture, and Structure
Material selection affects brand identity because customers interpret texture and structure as signals of quality and purpose. A washed 12 oz canvas tote suggests something very different from a crisp lightweight nylon organizer. Smooth microfiber, textured Oxford, ripstop nylon, pebbled PU, coated TPU, and genuine leather all communicate different product personalities even before customers understand the technical specification.
Fabric weight needs to fit the product rather than follow one collection-wide number. Lightweight organizers and linings commonly use lower-denier woven materials, while backpacks and equipment bags often require heavier constructions. Canvas is frequently specified by ounces per square yard, leather by thickness and finish, and neoprene by foam thickness, so a brand cannot create a meaningful consistency system by comparing only one type of specification.
| Material | Common Applications | Typical Development Considerations |
|---|---|---|
| 210D–420D polyester or nylon | Linings, lightweight pouches, organizers | Weight, foldability, coating, color |
| 600D polyester or Oxford | Backpacks, duffles, utility bags | Abrasion, structure, coating, cost |
| 900D–1680D technical fabrics | Tool, tactical, heavy-duty products | Weight, stiffness, sewing difficulty |
| 8–16 oz canvas | Totes, lifestyle bags, casual travel products | Texture, shrinkage, dye variation |
| PU leather | Small goods, trims, fashion bags | Surface finish, backing, flexibility |
| Genuine leather | Premium bags and accents | Hide variation, thickness, finish |
| Neoprene | Sleeves, lunch bags, protective products | Thickness, stretch, lamination |
These are common practical ranges rather than universal standards. A higher denier, thicker leather, or heavier canvas does not automatically create a better product. Excess material can increase shipping weight, make sewing more difficult, create bulky seams, and reduce comfort. The right specification is the one that supports the intended structure while maintaining the desired brand feel.
Szoneier’s documented material capabilities cover polyester, nylon, Oxford, canvas, cotton, neoprene, leather, PU, PVC, TPU, EVA, mesh, RPET, linings, and functional materials, with material selection evaluated against structure, cost, weight, durability, appearance, and product positioning. For a multi-product program, that comparison process is more useful than simply trying to repeat one fabric everywhere.
Build a Material Family
Mature collections often use a material family rather than one exact substrate. A technical travel brand might specify low-gloss woven surfaces, clean texture, matte hardware, and limited contrast. A lifestyle brand may prefer washed canvas, cotton webbing, warm neutral linings, leather details, and softer structures. An outdoor brand might lean toward coated nylon, molded patches, durable webbing, and restrained technical hardware.
A material-family definition becomes especially useful when a new product requires different performance. A laptop backpack may need substantial abrasion resistance and padding, while a packing cube should stay lightweight and compressible. They can use different fabrics yet still feel related because surface character, colors, trims, logo language, and finish remain within the established product family.
This approach also makes sourcing more resilient. Exact fabrics may become unavailable, suppliers may discontinue a weave, or a brand may need a lower-cost version for another channel. When the original material direction has been clearly documented, alternatives can be evaluated against appearance, hand feel, structure, thickness, durability, coating, logo compatibility, MOQ, lead time, and cost instead of being selected by fabric name alone.
Material selection is rarely a simple choice between “better” and “worse.” It is normally a balance among appearance, performance, manufacturing difficulty, minimum quantities, price, delivery timing, and repeatability. The strongest product development teams make those trade-offs deliberately and record what was accepted so later SKUs can follow the same logic.
How Do You Keep Logos Consistent?
Logo consistency depends on controlling master artwork, permitted variations, scale, placement, color, and physical production methods. The same technique or physical dimension does not need to appear on every product. Embroidery, printing, woven labels, molded patches, debossing, metal plates, and engraved pullers can coexist successfully when they preserve the same proportions, hierarchy, visual weight, and recognizable brand character.
Match the Process to the Material
Different branding methods have different physical limits, and ignoring those limits is one of the easiest ways to weaken brand consistency. Embroidery produces texture and depth, but very small lettering can close up. Screen printing can work well on many flat woven materials, yet coating and surface texture affect adhesion and clarity. Heat transfer can reproduce fine graphics, but the substrate must tolerate heat and pressure.
Rubber and silicone patches are useful on outdoor and technical products because they produce clear, durable shapes, but extremely fine lines and tiny letters may not mold cleanly. Woven labels handle compact branding well, while genuine leather and PU can support debossing, printing, foil stamping, laser work, or metal attachments depending on the desired finish.
A single collection may therefore use several methods without looking inconsistent. A backpack could use a rubber patch, a toiletry pouch a woven label, a PU organizer a debossed logo, a canvas tote embroidery, and a zipper puller an engraved symbol. The manufacturing techniques differ, but the underlying artwork, proportions, spacing, and prominence can remain closely related.
Szoneier’s documented branding processes include screen printing, heat transfer, digital printing, sublimation, embroidery, woven labels, leather patches, rubber and silicone patches, metal plates, debossing, hot stamping, laser engraving, reflective branding, jacquard webbing, and customized zipper pullers. The same documentation notes that material, logo detail, color requirements, MOQ, durability, cost, and bulk-production stability should influence process selection.
Control Scale and Placement
Using one fixed logo width across every SKU rarely produces a balanced range. A 70 mm mark can look modest on a large travel bag and oversized on a compact pouch. The more useful standard is proportional visual weight, supported by SKU-specific dimensions that are recorded after the sample has been evaluated.
Small accessories often use compact logos in the approximate 20–40 mm range, medium bags may work with 40–70 mm applications, and larger duffles or backpacks may support 70–100 mm or larger branding. These numbers are practical starting points rather than universal standards because logo shape, surrounding space, process, bag dimensions, and desired visibility can change the correct result considerably.
Placement can be standardized through zones. Small pouches might use an upper-center or lower-corner mark. Backpacks may use the front-pocket center or upper front panel. Duffles often work well with a broad side-panel position, while small leather goods may use restrained corner branding or an interior mark. Exact measurements should then be placed in each product specification.
Brands should also control the number of branding points. A front logo, branded zipper pullers, jacquard straps, printed lining, side label, and oversized hangtag may all follow the same identity, yet using every element at once can make the product feel promotional. Consistency is usually more convincing when the hierarchy is deliberate and customers can recognize the brand without seeing the logo repeated on every available surface.
Approve Physical Branding
An approved vector file is not the same thing as an approved physical logo. Artwork can be mathematically correct while the embroidery becomes too dense, the rubber border is too thick, a metal plate reflects too much light, or a woven label loses small details. Production approval must therefore happen on the real material at a realistic size.
Useful physical checks include finished dimensions, letter clarity, line thickness, color, edge quality, surface finish, attachment method, placement, and durability. When tooling is involved, such as molded patches or customized metal pullers, product teams should also confirm how small details translate into the tooling process before authorizing larger production quantities.
Small applications are particularly sensitive. A fine 0.3 mm graphic line that works perfectly in print may not reproduce reliably in molded rubber, embroidery, weaving, or engraving. Simplification can be necessary, but it should be controlled by the brand rather than improvised independently by every factory or trim supplier.
For this reason, serious product programs benefit from maintaining several approved artwork forms: the full master logo, a simplified small-scale version, a single-color version, and any reversed version needed for dark substrates. Those files provide suppliers with controlled alternatives and reduce the risk that the brand mark changes gradually as it moves from one component and manufacturing technique to another.
How Do You Control Multiple Bag SKUs?
Multiple bag SKUs are easier to control when one master brand system is connected to individual product specifications. Shared colors, materials, logo files, hardware finishes, labels, packaging rules, and component references should be managed centrally, while each SKU keeps its own tech pack, BOM, sample record, barcode information, and revision history. This reduces duplicated decisions and improves consistency during launches and reorders.
Master Standards and Product Files
Once a collection expands beyond three or four styles, email threads and memory become poor product-management systems. A master standard should contain everything shared across the range, including colors, logo files, hardware direction, labeling, packaging architecture, material character, and key workmanship expectations. The individual SKU file then records dimensions, construction, materials, component codes, branding position, and packaging dimensions for that product.
This division reduces repeated decision-making. Consider an eight-style collection with three colors and two packaging channels. That creates as many as 48 style-color-channel combinations. If every combination is described informally, artwork mistakes, component substitutions, label errors, and packaging confusion become increasingly likely as several orders move through development at the same time.
A simple coding system can make the range easier to control. A reference such as TR01-NV-US-V03 might indicate style TR01, navy color, US packaging, and revision 03. Another company might use a completely different code. The specific format matters less than applying the same structure across development, production, inspection, warehousing, and future reorders.
Version control should also extend to artwork. Once a product is approved, the active specification should clearly identify the current version while obsolete files are archived away from the
Tech Packs, BOMs, and Samples
A tech pack explains how the product should be built. A bill of materials identifies the materials and components required to build it. An approved physical sample shows how the complete combination should look and feel. None of these references replaces the others, and strong product programs use all three together.
A reasonably detailed bag BOM may contain shell fabric, lining, reinforcement, foam, zipper chain, sliders, pullers, webbing, buckles, hooks, D-rings, thread, labels, logo components, and packaging. A backpack containing 20 significant material or component references across six SKUs can already involve around 120 BOM-level items, even before color variants and packaging versions are considered.
That volume explains why casual substitutions cause problems. Changing a zipper slider may alter plating and perceived quality. Replacing webbing can change texture and shade. A different foam thickness may noticeably change the silhouette. A revised lining can affect hand feel and weight. Every one of those decisions can move the product slightly away from the established collection.
The approved physical sample is valuable because it captures information that is difficult to communicate numerically. A technical document can record a fabric code and dimensions, but the sample shows overall stiffness, visual proportion, shape, hand feel, logo balance, and the relationship among trims. For important programs, a clearly identified approved or pre-production sample should remain part of the production reference.
Manage Variants as a System
Color variants multiply more than shell-fabric decisions. A black version of a bag may require coordinated shell, zipper tape, webbing, thread, lining, logo, puller, and hardware selections. A sand version may use tonal variations, while a bright seasonal color can require custom-dyed zipper tape or specific logo colors.
A simple SKU matrix can prevent these relationships from being lost.
| Field | Example |
|---|---|
| Style | Travel Pouch |
| Style Code | TP01 |
| Color | Navy |
| Shell | 420D Nylon |
| Lining | 210D Polyester |
| Logo | Rubber Patch A |
| Hardware | Matte Black |
| Packaging | Retail Polybag |
| Barcode | SKU-specific |
| Approved Sample | TP01-NV-V02 |
Suppose a collection includes five styles, three colors, and two logo variations. The program may involve up to 30 style-color-logo combinations. Add regional packaging or channel-specific barcodes and the number rises again. This is manageable when variants are designed inside one architecture; it becomes difficult when every combination is treated as a separate custom project.
Shared materials and components can reduce both sourcing complexity and visual variation. A backpack, travel pouch, and toiletry bag might share shell material, zipper family, puller finish, and labeling while retaining different structures. Szoneier’s internal project documentation notes that mixed-style and multi-SKU programs can be evaluated according to material sharing, structure, logo process, packaging, and production complexity.
However, sharing components does not automatically mean sharing every MOQ. Fabric dyeing, customized hardware, printed labels, molded logos, and packaging can each have their own production minimums. Collection planning should therefore be evaluated both at SKU level and at shared-component level before quantities are finalized.
Reorders Need Their Own Discipline
The second production run often reveals whether a brand has built a genuine product system. The original order may receive intense attention because every decision is new. Six or twelve months later, a different material batch, revised trim supplier, updated package, new sewing line, or changed staff member can introduce small differences that nobody intended.
A reorder package should therefore preserve the latest tech pack, BOM, artwork, material references, approved color, trim references, packaging files, SKU codes, inspection criteria, revision history, and approved physical sample. The team should compare each new production setup against that package rather than relying on the phrase “same as last order.”
This is especially important for growing brands. A new pouch may share the original backpack’s zipper, fabric, puller, webbing, and packaging architecture. If the previous standards have been archived properly, the new development begins from proven references. If they have not, every extension becomes another opportunity for the collection to drift.
The objective is not to stop products from evolving. Strong products improve over time. A better buckle, revised lining, strengthened seam, or more efficient packaging can all be worthwhile updates. The important distinction is that the change becomes a new approved version rather than quietly entering production without a clear record.
How Does Manufacturing Protect Brand Consistency?
Manufacturing protects brand consistency by turning design decisions into approved materials, physical samples, measurable specifications, production checkpoints, and repeatable reorder references. Effective control catches differences in color, hardware, branding, dimensions, stitching, labels, and packaging before those differences are repeated throughout a large order. The strongest systems compare production against approved references from incoming materials through final packing.
Pre-Production Approval
Many problems that later appear to be QC failures actually begin as unresolved product-development decisions. If no one has defined the approved hardware finish, an inspector cannot confidently determine whether a new finish is wrong. If the logo position has never been measured, production staff have no objective placement standard. Quality control cannot compensate for missing specifications.
Before bulk sewing begins, important categories should normally be confirmed, including shell material, lining, color, zipper, webbing, hardware, branding, dimensions, construction, labels, packaging, and the final approved sample. Even a comparatively straightforward bag can therefore contain 12 or more major approval areas before detailed seam, reinforcement, pocket, and workmanship requirements are considered.
For six SKUs, ten significant approval areas already create at least 60 product-level decisions. That is one reason written approval records are more valuable than verbal confirmation. They reduce ambiguity among designers, sourcing staff, factories, inspection teams, and the colleagues responsible for a reorder months later.
A pre-production sample is particularly useful when the original prototype has passed through several revisions. It confirms that the production team is preparing to manufacture the final accepted construction rather than an earlier version that happens to look similar in photographs.
Incoming and In-Process Control
Waiting until all products are finished is an expensive way to discover that a zipper, logo component, or webbing color is incorrect. Incoming inspection can identify discrepancies in shell material, fabric shade, coating, zipper tape, sliders, webbing, hardware plating, labels, molded branding, and packaging materials before those components are incorporated into hundreds or thousands of finished products.
Once production begins, control shifts toward execution. Logo placement, seam alignment, pocket position, strap symmetry, hardware orientation, zipper installation, dimensions, reinforcement, and construction details can be checked against specifications and the approved sample. Problems discovered at this stage are usually easier to correct than the same problems found after the products have been fully assembled and packed.
Szoneier’s documented QC process includes raw material inspection, accessory inspection, pre-production sample confirmation, cutting inspection, sewing-process checks, semi-finished inspection, final product inspection, and packaging inspection. This layered approach is useful for brand consistency because visual and component mistakes are more economical to correct before they have been repeated across the full production quantity.
A simple promotional pouch can require the same discipline as a premium handbag when volume is high. A slightly incorrect logo color repeated over 20,000 units can create a larger commercial problem than a small workmanship defect on a low-volume luxury program. Control should therefore reflect the significance and repeatability of the issue, not only the product’s retail price.
Final Product and Packaging Control
Final inspection should look beyond whether seams are straight and zippers function. For brand consistency, finished goods should also be compared with approved references for overall appearance, color relationship, logo size, logo placement, hardware finish, zipper pullers, webbing, lining, dimensions, visible stitching, labels, packaging, and SKU identity.
Color should receive particular attention when production uses several fabric rolls or material batches. Two shades can appear acceptable when viewed separately and become clearly different when products are displayed side by side. If products from multiple batches will appear together in retail or online photography, the visual relationship matters as much as the individual acceptance of each roll.
Packaging identity also belongs inside quality control. A well-manufactured product packed in the wrong SKU bag or given the wrong barcode can cause inventory problems, incorrect fulfillment, customer returns, and poor reviews. As assortments grow, confirming the relationship between product, color, barcode, hangtag, polybag, carton label, and shipment information becomes increasingly important.
The finished inspection should therefore protect both physical product quality and commercial identity. The goal is not simply to confirm that the factory made a functioning bag. It is to confirm that the product reaching the customer is the same brand-approved SKU that everyone intended to produce.
Production Memory Protects the Next Order
A reliable manufacturing relationship should retain the practical memory of a successful product. That memory includes approved patterns, BOM versions, material references, color direction, artwork, branding tooling, package files, QC records, and physical reference samples. These records become increasingly valuable when a collection grows from two or three products into a broader family.
Szoneier’s manufacturing position is built around helping brands move from product ideas and samples to controlled bulk production while maintaining stronger sample-to-bulk consistency and supporting long-term product development. For a brand building several related accessories, that continuity can matter as much as the first prototype because customers judge consistency over repeated purchases, not only during the initial launch.
The purpose of production memory is not to prevent improvement. Materials change, markets change, packaging evolves, and product construction can be refined after customer feedback. What matters is that those changes are deliberate and traceable. A revised zipper or improved lining should become part of a new approved version, not an undocumented substitution that quietly changes the product.
That distinction between controlled evolution and uncontrolled variation is what allows a brand to keep expanding. Products can become lighter, stronger, easier to manufacture, or more cost-efficient without losing the characteristics that customers already recognize.
Brand consistency across bag accessories is ultimately a discipline of controlled translation. A brand identity may begin as colors, logos, typefaces, design references, and positioning, but customers experience it as fabrics, hardware, zippers, stitching, labels, packaging, hand feel, product proportions, and repeatable quality. The larger the collection becomes, the less reliable informal decision-making becomes.
The strongest product ranges define what should remain recognizable, allow function-driven differences where they make sense, evaluate colors on real materials, choose logo methods according to the substrate, record shared components, approve physical samples, and compare bulk production with those references. Those habits are not glamorous, but they are what keep an eight-SKU collection from slowly turning into eight unrelated products.
For brands developing a new accessory collection or extending an existing bag line, Szoneier can participate from material and component selection through sampling, logo application, production coordination, QC, packaging, and repeat-order planning. The practical value is not simply having more customization options. It is being able to translate one brand direction into different physical products while keeping the collection recognizable, manufacturable, and repeatable as the range grows.
Frequently Asked Questions
How do you maintain brand consistency across different bag materials?
Brand consistency across different materials comes from controlling the relationship among color, texture, sheen, logo treatment, trims, hardware, and finishing rather than demanding that every substrate look identical. A Pantone reference can establish direction, but nylon, canvas, PU, webbing, rubber, and metal should still be reviewed physically. Approved swatches and final samples provide a more reliable production reference than screen colors alone.
Should every bag in a collection use the same material?
No. Using the same material across every SKU can reduce functionality and make some products unnecessarily heavy, expensive, stiff, or difficult to manufacture. A better approach is to build a material family with related colors, surface character, texture, and perceived quality. A backpack, pouch, wallet, and luggage tag can use different substrates while remaining visually connected through common branding, trims, hardware, and finishing.
Should logo size be the same across all bag accessories?
Logo dimensions normally need to change according to product size, available panel area, process limitations, and intended visual prominence. A small pouch might use a 20–40 mm mark, while a larger backpack or duffle can accommodate considerably more. These are only reference ranges. What should remain consistent is the logo’s proportions, hierarchy, color direction, and relative visual weight rather than one universal measurement.
Which logo methods are best for a coordinated bag collection?
There is no single logo process that works best across every product. Embroidery suits many textile applications, woven labels work well at smaller scales, rubber or silicone patches fit many outdoor products, and debossing or metal branding can work well on PU and leather goods. The strongest collections select methods according to material and product function while keeping master artwork, proportions, colors, and placement logic controlled.
How can brands prevent color differences in bulk bag production?
Color variation can be reduced through physical color references, approved swatches, sample confirmation, material-batch checks, zipper and webbing matching, logo-color approval, and comparison with the approved sample before shipment. Some variation is natural across different substrates and dyeing processes, so the objective should be a controlled and intentional visual relationship rather than assuming that one digital color number guarantees identical physical results.
What documents help keep multiple bag SKUs consistent?
The most useful records are a master brand specification, individual tech packs, bills of materials, approved artwork, color and material references, SKU codes, packaging files, revision history, QC criteria, and retained approved samples. A master system controls elements shared across the collection, while SKU-level files document the construction and component differences required by each product. Together, they create a clearer reference for sampling, production, inspection, and reorders.
How can a manufacturer help maintain consistency on repeat orders?
A manufacturer can support repeatability by retaining the latest approved specifications, patterns, materials, artwork, component references, packaging files, QC standards, and sample history, then checking the next order against those references before production begins. Repeat orders should not rely on memory or the phrase “same as last time.” A documented comparison makes legitimate improvements visible and helps prevent unnoticed substitutions from gradually changing the product.